
The Short Answers
- A standard #30 drill bit (0.1285") is the most common choice for tapping a 10-32 thread in steel or aluminum.
- For softer materials (brass, plastic), use a #29 (0.136") to prevent thread stripping.
- Always check your tap’s manufacturer specifications—some high-performance taps recommend 0.127" or 0.129" for better clearance.
- Blind holes require a counterbore to avoid breaking the tap; the drill depth should be 75% of the thread length.
- If threads are binding, increase the drill size by 0.001" increments until the tap runs freely.
Deep Dive: The Full Picture
The 10-32 thread is a workhorse in mechanical assemblies, balancing strength and fine adjustment. Its small diameter makes it ideal for delicate components, but the tight tolerances demand precision. The drill bit size isn’t just a static number—it’s a function of the tap’s cutting angle, the material’s ductility, and whether you’re tapping through or blind. For example, a hand tap (used manually) may require a slightly larger pilot hole than a machine tap (used with power tools), because hand taps rely more on the material’s ability to deform around the threads.
Most tap drill charts simplify the answer to #30 (0.1285") for 10-32, but this assumes medium-hard steel as a baseline. The reality is more nuanced: softer metals like aluminum or brass will deform more easily, so a #29 (0.136") might be safer to prevent thread stripping. Conversely, hardened steel or stainless may need a #31 (0.120") to avoid tap breakage. Even within the same material, variations in heat treatment or grain structure can alter the optimal drill size. This is why machinists often carry a set of drill bits and test the first few threads before committing to a full run.
#### The Context You Need
The 10-32 thread is part of the Unified National Fine (UNF) series, which prioritizes finer pitches for smaller diameters. Unlike coarse threads (UNC), which are designed for quick assembly/disassembly, fine threads like 10-32 are used where precision alignment or fine adjustment is critical—think camera mounts, aerospace fittings, or medical devices. The tap drill size is derived from the minor diameter (the smallest diameter of the thread root) minus a clearance allowance to prevent the tap from bottoming out against uncut material. Historically, tap drill charts were standardized by organizations like the ANSI and ISO, but these were based on average material properties. In practice, a machinist might adjust the drill size based on empirical testing. For instance, if a 10-32 tap with a #30 pilot hole binds in 6061 aluminum, they might switch to a #29 and ream the hole slightly to achieve a cleaner thread. This trial-and-error approach is why tap-and-die sets often include multiple drill sizes for the same thread pitch. ####The Mechanics
When you tap a hole, the drill bit removes material to create a pilot hole that the tap will enlarge into threads. The tap’s cutting flutes remove chips and form the thread profile, but the initial hole must be slightly smaller than the tap’s major diameter (0.0625" for 10-32). The exact size depends on the tap’s lead angle and the material’s shear strength. A standard tap (60° point angle) will require a pilot hole closer to the minor diameter, while a high-speed tap (steeper angle) might need a marginally larger hole to reduce cutting forces. The formula for calculating the ideal tap drill size is: Tap Drill Diameter = Major Diameter – (Pitch × 0.6) For 10-32: - Major diameter = 0.0625" - Pitch = 1/32" = 0.03125" - 0.0625 – (0.03125 × 0.6) = 0.044375" This theoretical value rounds to ~0.044", but in practice, #30 (0.1285") is used because: 1. The formula assumes a perfect tap, but real taps have clearance angles that require a slightly larger hole. 2. Material elasticity means softer metals need more clearance to avoid galling. 3. Tap wear over time can increase the effective diameter, necessitating a larger pilot hole.Details That Change the Picture
Not all 10-32 taps are created equal. A hand tap designed for manual use might have a sharper point angle to bite into material more aggressively, while a machine tap (for power tools) often has a longer lead to reduce torque. This affects the optimal drill size: a hand tap may require a #30, but a machine tap could handle a #29 without binding. Additionally, thread depth matters—full-depth threads (like in fasteners) need precise clearance, whereas partial-depth threads (for alignment) can tolerate slightly larger pilot holes.
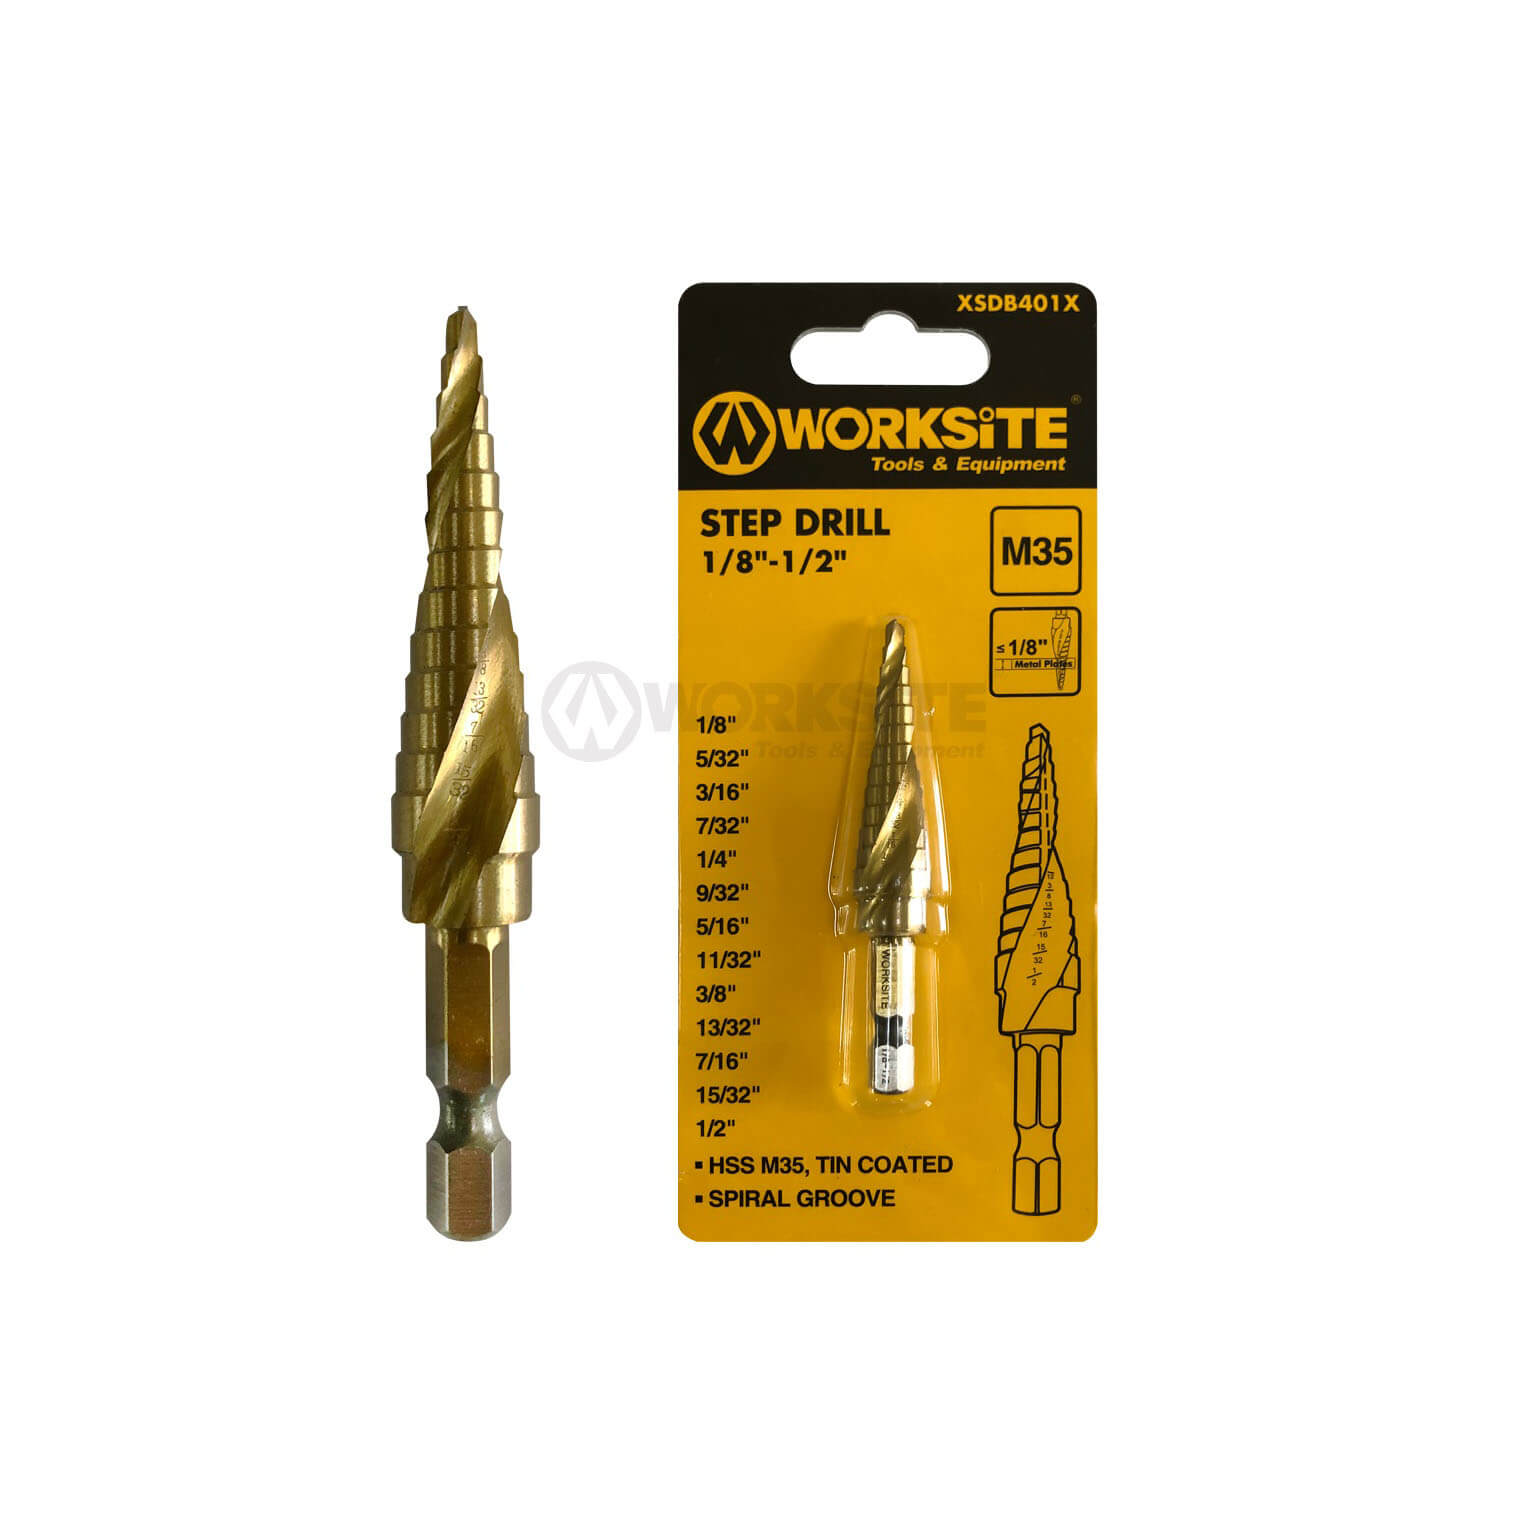
Another critical factor is hole depth. For through holes, the tap can exit cleanly, but for blind holes, the tap must bottom out without breaking. Here, the drill depth should be 75% of the thread length to prevent the tap from striking the hole bottom. If the hole is too shallow, the tap will bottom out prematurely, stripping threads or snapping. Some machinists use a step drill to create a counterbore at the bottom of blind holes, ensuring the tap has room to clear.
"You can’t tap a hole to perfection with a single drill size—it’s part science, part art. Start with the chart, but always test the first few threads. If the tap drags, you’re too tight; if the threads are weak, you’re too loose." — Mark Reynolds, Master Machinist (30+ years in aerospace tooling)
| Material | Recommended Drill Bit (10-32 Tap) |
|---|---|
| Steel (mild, A36) | #30 (0.1285") |
| Aluminum (6061, 2024) | #29 (0.136") or #30 |
| Stainless Steel (304, 316) | #31 (0.120") or #30 |
| Brass/Plastic | #29 (0.136") |
Conclusion
The question what size drill bit for 10-32 tap? doesn’t have a one-size-fits-all answer, but #30 (0.1285") is the safest starting point for most applications. The key is understanding that material properties, tap design, and hole type all influence the optimal size. If you’re working with high-tolerance components, consider consulting a tap drill chart from your tap manufacturer—some high-performance taps (like those from HSS or carbide-coated brands) specify slightly larger pilot holes for better chip evacuation.
For beginners, the best approach is to start with the chart, test the first few threads, and adjust as needed. If threads are binding, increase the drill size in 0.001" increments until the tap runs smoothly. For professionals, calibrated drill bits and tap-and-die sets with included charts streamline the process. Remember: a properly tapped hole isn’t just about the right drill bit—it’s about clearance, depth, and material behavior. Master these, and you’ll avoid the frustration of stripped threads or broken taps.
Comprehensive FAQs
#### Q: Why does the recommended drill bit vary for 10-32 taps?
The variation comes from material hardness, tap design, and thread depth. Softer metals (like aluminum) deform more easily, so a larger pilot hole (#29) prevents stripping. Harder metals (like stainless) require a smaller hole (#31) to avoid tap breakage. Additionally, hand taps vs. machine taps have different lead angles, affecting clearance needs.
####Q: Can I use a #30 drill bit for 10-32 in all materials?
#30 (0.1285") is a general-purpose choice, but it’s not universal. For brass or plastic, a #29 (0.136") is safer to prevent thread stripping. For hardened steel or stainless, a #31 (0.120") may be needed to avoid tap binding. Always test the first few threads and adjust if necessary.
####Q: What if my tap keeps breaking when using a #30 for 10-32?
Breaking taps usually indicate insufficient clearance or poor lubrication. Try increasing the drill size to #29 (0.136") and use a tap fluid or cutting oil. If the material is extremely hard (e.g., tool steel), consider a carbide-coated tap or a step-down approach (start with a smaller drill, then ream).
####Q: Do I need a special drill bit for tapping blind holes?
No, but you must control depth to prevent tap breakage. Drill the hole to 75% of the thread length, then use a counterbore or spot-facing tool to create clearance for the tap’s bottom. For example, a 1/4" deep thread should have a hole drilled to 3/16" before tapping.
####Q: Is there a difference between metric and imperial tap drill sizes for 10-32?
Yes. A 10-32 tap is imperial, and its metric equivalent is M3.5 × 0.6 (3.5mm diameter, 0.6mm pitch). The tap drill for M3.5 is ~3.0mm, which converts to ~0.118", closer to a #32 drill bit (0.121"). Always use imperial or metric consistently—mixing them risks incorrect thread formation.
####Q: Can I use a step drill to create the pilot hole for a 10-32 tap?
Yes, but precision matters. A step drill can create a counterbore or chamfer, which helps guide the tap. However, ensure the final diameter matches your tap drill chart—step drills often jump in 0.010" increments, which may be too coarse for fine threads like 10-32.
####Q: What’s the best way to verify my tap drill size is correct?
Use a micrometer or caliper to measure the drilled hole before tapping. The diameter should match your chosen drill bit’s specification (e.g., #30 = 0.1285"). For critical applications, test-fit the tap—it should enter the hole without excessive drag but still form clean threads. If the tap spins freely with no resistance, the hole may be too large.
####Q: Are there any online tools to calculate tap drill sizes?
Yes, several free calculators exist, such as those from TapMaster, Tap Drill Size Calculator, or Machinist’s Handbook apps. Input your thread size (e.g., 10-32) and material, and they’ll suggest the optimal drill bit. However, always cross-check with a physical tap drill chart—online tools can vary in accuracy.
