
Where It All Began
The origins of ultrasonic cleaner solutions for aluminum trace back to the 1950s, when ultrasonic cleaning was first adapted from medical and dental applications. Early systems used frequencies around 20–50 kHz, effective for removing organic debris but too aggressive for aluminum’s oxide layer. The breakthrough came when researchers at the Battelle Memorial Institute experimented with lower-power, higher-frequency transducers. Their work showed that 40 kHz could generate enough cavitation to lift contaminants without pitting the metal—a critical insight for industries where surface integrity mattered. The first commercial cleaner solutions for aluminum appeared in the 1970s, tailored for electronics manufacturing. These early formulations relied on water-based detergents with mild alkalis, designed to dissolve oils and particulates without attacking the metal. However, they lacked the precision needed for aerospace or medical-grade aluminum. The real inflection point arrived when manufacturers began adding corrosion inhibitors like sodium nitrite or benzotriazole to stabilize the aluminum surface during cleaning.The Early Signs
By the late 1980s, jewelers and watchmakers were quietly adopting ultrasonic cleaning solutions for aluminum for their ability to restore intricate engravings without manual polishing. The process revealed something unexpected: aluminum’s natural oxide layer, when properly preserved, could act as a protective barrier against further corrosion. This led to the development of post-cleaning rinses with de-ionized water and mild acid neutralizers, ensuring the metal’s longevity. Meanwhile, in industrial settings, the limitations became clear. High-frequency ultrasonic cleaning could strip anodized coatings if the solution’s pH drifted above 9.5. The industry’s response? A shift toward pH-balanced cleaner solutions for aluminum with built-in buffering agents, like sodium bicarbonate or citric acid. These adjustments turned ultrasonic cleaning from a gamble into a controlled process—one that could be documented, replicated, and optimized.The Turning Point
The moment ultrasonic cleaner solutions for aluminum transitioned from novelty to necessity was when aerospace engineers realized traditional cleaning methods couldn’t keep pace with miniaturization. In the late 1990s, satellite manufacturers faced a dilemma: how to clean micro-fabricated aluminum components without introducing contaminants that could interfere with electromagnetic sensors. The answer lay in ultrasonic cleaning solutions for aluminum with frequencies above 100 kHz, capable of targeting specific residue types without affecting the base metal. The shift wasn’t just about frequency. It was about chemistry. Engineers at Boeing and Lockheed Martin collaborated with detergent manufacturers to develop formulations that could remove flux residues from soldered aluminum joints while preserving the integrity of the anodized surfaces. The result? A new standard for cleanliness in critical applications, where even microscopic particles could compromise performance."We weren’t just cleaning aluminum—we were cleaning the future of flight. The difference between a 99% clean part and a 99.99% clean part, in some cases, is the difference between success and failure." — Dr. Elena Vasquez, Materials Science Lead, NASA JPL (2003)

The Build-Up, Year by Year
| Period | Key Developments |
|---|---|
| 1995–2000 | Introduction of pH-stabilized ultrasonic cleaner solutions for aluminum for electronics manufacturing. First use in medical device sterilization (e.g., surgical instrument trays). |
| 2000–2005 | Aerospace adoption accelerates with high-frequency ultrasonic cleaning solutions for aluminum (80–120 kHz) for satellite components. First proprietary formulations with corrosion inhibitors. |
| 2010–Present | Rise of eco-friendly ultrasonic cleaner solutions for aluminum (e.g., biodegradable surfactants, reduced-water systems). Integration with automated cleaning cells in automotive and renewable energy sectors. |
Lessons From the Journey
- Frequency matters, but not linearly. While higher frequencies (above 100 kHz) excel at delicate work, lower frequencies (25–40 kHz) are better for heavy-duty cleaning of thick aluminum castings.
- Aluminum’s alloy composition dictates the solution. 2024-T3 (high-strength aircraft alloy) requires different inhibitors than 3003-H14 (soft sheet metal).
- Rinsing is the unsung hero. A single rinse cycle with de-ionized water can remove up to 90% of residual detergent, preventing post-cleaning corrosion.
- Temperature control is non-negotiable. Solutions above 60°C can degrade certain surfactants, while temperatures below 20°C reduce cavitation efficiency.
- Automation reduces human error. Modern systems now include ultrasonic cleaner solution for aluminum monitoring for pH, conductivity, and inhibitor levels in real time.
Where Things Stand Today
Today, ultrasonic cleaner solutions for aluminum are no longer a specialized tool but a cornerstone of industries where precision cleaning meets material sensitivity. In jewelry, custom formulations now include nanoparticle-enhanced detergents that target oxidation at the molecular level without affecting gemstone settings. Meanwhile, automotive manufacturers use ultrasonic cleaning solutions for aluminum to restore anodized wheel rims without compromising the ceramic coating’s adhesion. The most significant evolution, however, is in sustainability. Older formulations relied on harsh solvents like trichloroethylene, now banned in many regions. Modern eco-conscious ultrasonic cleaner solutions for aluminum use plant-based surfactants and closed-loop water systems, reducing waste by up to 80%. This shift reflects a broader trend: ultrasonic cleaning for aluminum is now as much about environmental responsibility as it is about performance.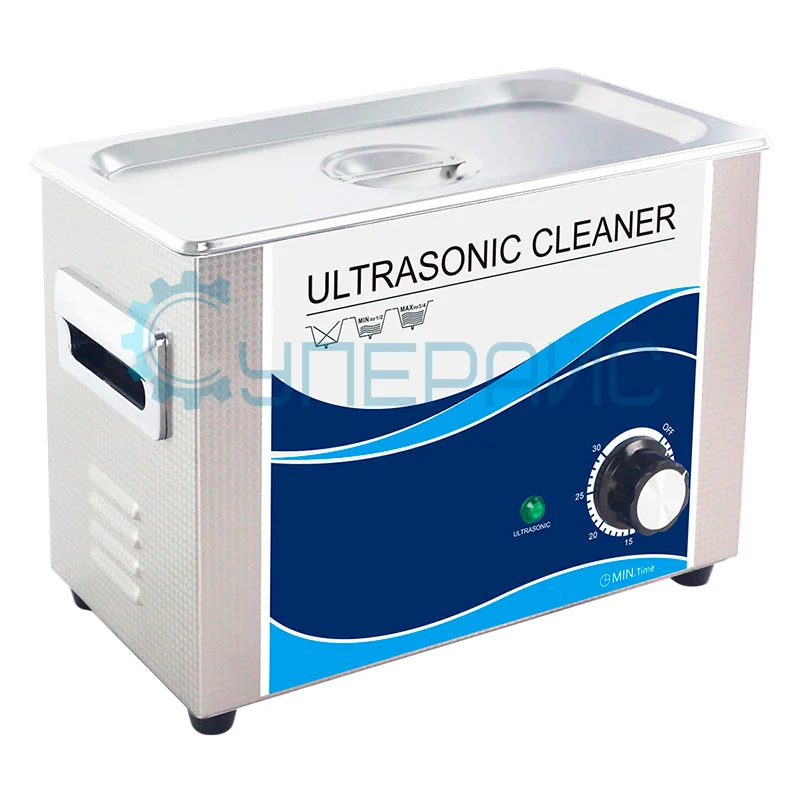
Conclusion
The story of ultrasonic cleaner solutions for aluminum is one of incremental innovation disguised as routine maintenance. What began as a workaround for a jeweler’s tarnished cufflinks has become a science—one that balances chemistry, physics, and material science. The key takeaway? There’s no one-size-fits-all cleaner solution for aluminum. The right approach depends on the alloy, the application, and the end goal: whether it’s restoring a 1920s Art Deco brooch or ensuring a Mars rover’s landing gear remains pristine. As industries push the boundaries of what aluminum can endure—from hypersonic aircraft to offshore wind turbines—the demand for specialized ultrasonic cleaning solutions for aluminum will only grow. The challenge isn’t just cleaning; it’s preserving. And in that tension lies the future of the process.Comprehensive FAQs
Q: Can I use a generic ultrasonic cleaner with any ultrasonic cleaner solution for aluminum?
No. Generic cleaners often use frequencies or power levels incompatible with aluminum’s oxide layer. For example, a dental cleaner (typically 28–45 kHz) may pit soft aluminum alloys, while a jewelry cleaner (80–120 kHz) might not adequately remove heavy grease. Always match the ultrasonic cleaner solution for aluminum to the transducer frequency and power output specified by the manufacturer.
Q: What’s the safest cleaner solution for aluminum for home use?
For non-industrial applications, a mild pH-balanced ultrasonic cleaner solution for aluminum (pH 7–9) with a corrosion inhibitor like sodium gluconate is safest. Avoid citrus-based cleaners (e.g., lemon juice), which can accelerate oxidation. Brands like Jeweler’s Ultimate or Alconox offer pre-formulated options designed for home ultrasonic baths.
Q: How do I know if my ultrasonic cleaner solution for aluminum is contaminated?
Signs include:
- Cloudy or discolored solution (indicates metal ions or detergent breakdown).
- Reduced cavitation (visible as fewer bubbles or weaker agitation).
- Aluminum parts appearing dull or streaked post-cleaning.
Q: Does ultrasonic cleaning remove anodized coatings from aluminum?
Not inherently—but improper ultrasonic cleaner solutions for aluminum can. Anodized coatings (e.g., Type II or III) are porous and can absorb aggressive detergents or high-pH solutions. To preserve anodization:
- Use pH-neutral or slightly acidic solutions (pH 5–7).
- Limit cleaning time to 2–5 minutes.
- Avoid frequencies above 80 kHz for thick anodized layers.
Q: Are there ultrasonic cleaner solutions for aluminum that work for both jewelry and aerospace?
Rarely. Jewelry-focused ultrasonic cleaner solutions for aluminum prioritize mild detergents to avoid damaging gemstones, while aerospace formulations include stronger inhibitors (e.g., benzotriazole) to prevent stress corrosion cracking in high-strength alloys. A compromise exists for general-purpose cleaning (e.g., Alconox Powdered Cleaner), but critical applications require alloy-specific solutions.
Q: How does temperature affect ultrasonic cleaner solutions for aluminum?
Temperature influences cavitation and chemical reactivity:
- Below 20°C: Reduced cavitation efficiency; detergents may precipitate.
- 20–40°C (optimal range): Balances cleaning power and solution stability.
- Above 60°C: Can degrade surfactants, accelerate oxidation, or cause inhibitor breakdown. Most ultrasonic cleaner solutions for aluminum specify a max temperature of 45–50°C.
