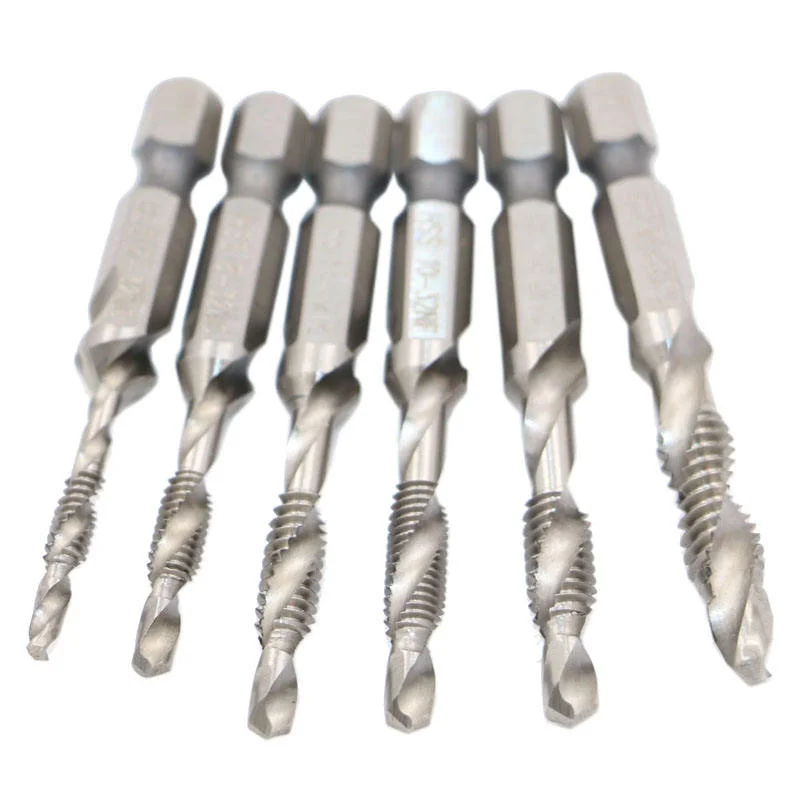
The 10/32 tap drill bit size is a metric that separates precision work from guesswork in threading operations. At its core, it represents a fraction of an inch—0.3125 inches—that dictates the diameter of the pilot hole required before tapping a 10-32 thread. This seemingly simple measurement is the linchpin of repeatable, high-quality threads in everything from aerospace components to consumer electronics. Yet its importance is often overshadowed by broader discussions on tap sizes, leaving practitioners to rely on outdated charts or trial-and-error methods.
The relationship between tap size and drill diameter isn’t arbitrary. It’s governed by material properties, thread pitch, and the mechanical stress a thread must endure. A miscalculation here—whether using a 10/32 tap drill bit size that’s too large or too small—can lead to stripped threads, weakened joints, or even catastrophic failures in structural applications. The stakes are higher than most realize, especially in industries where thread integrity directly impacts safety or performance.
What follows is an analysis of how the 10/32 tap drill bit size is derived, its verified applications, and the variables that influence its selection. The focus remains on empirical data and industry standards, not speculative trends.

Breaking Down the Numbers
The 10/32 tap drill bit size is derived from a fundamental principle: the minor diameter of a thread must accommodate the tap’s cutting flutes while leaving sufficient material for the root strength of the thread. For a 10-32 thread (10 threads per inch), the standard drill size isn’t simply the major diameter minus the pitch. Instead, it accounts for the tap’s land width, the thread’s depth, and the material’s tolerance for deformation.
Industry tables—such as those from the
American National Standards Institute (ANSI) or ISO 261—provide baseline recommendations. For a 10-32 tap, the nominal drill size is 0.281 inches (7.14 mm), not the 0.3125 inches of the 10/32 fraction itself. This discrepancy arises because the 10/32 measurement refers to the major diameter of the thread, while the drill size targets the root diameter after tapping. The confusion between these two figures is a common pitfall in workshops where precision is critical.
####
The Verified Baseline
Publicly available machining handbooks confirm that the
10/32 tap drill bit size for a standard 10-32 thread is 0.281 inches (7.14 mm). This value is consistent across major standards bodies, including ANSI B1.1 and ISO 261, which specify thread dimensions for Unified and metric threads. The calculation is based on:
1. Major diameter (10/32 = 0.3125") – The outer diameter of the thread.
2. Pitch (32 threads per inch) – The distance between thread crests.
3. Thread depth – Typically 50% of the pitch for Unified threads, yielding a depth of 0.0156 inches.
4. Drill allowance – A slight undersize (0.002–0.003") to prevent binding during tapping.
The
0.281-inch figure emerges from subtracting twice the thread depth from the major diameter, adjusted for tap clearance. This is the drill size that ensures the tap can cut cleanly without excessive force or material tear-out.
####
What the Estimates Suggest
Industry estimates suggest that
deviations from the 0.281-inch baseline—whether due to material hardness, tap wear, or non-standard thread forms—can introduce variability. For example:
- Soft materials (e.g., aluminum, brass): Some machinists opt for a 0.284-inch drill to compensate for thread compression during tapping.
- Hardened steels: A 0.278-inch drill may be used to prevent tap breakage under high torque.
- Custom threads (e.g., fine-pitch): The effective drill size might shift to 0.275–0.285 inches depending on the thread angle and flute design.
These adjustments are
not standardized but reflect practical experience in specialized applications. The key takeaway: while the 10/32 tap drill bit size is theoretically 0.281 inches, real-world conditions often demand slight modifications.
Case Study: A Closer Look
In aerospace manufacturing, a subcontractor faced recurring issues with 10-32 threads in titanium alloy components. Initial attempts used a
0.281-inch drill, but the threads frequently stripped during assembly. Upon analysis, metallurgists determined that titanium’s low thermal conductivity caused localized heating during tapping, softening the material and increasing thread deformation.
The solution? A
0.276-inch drill paired with a high-speed, lubricated tap. This reduced the effective thread depth slightly, preventing over-cutting while maintaining sufficient engagement. The adjustment shaved 0.005 inches from the nominal size—a seemingly minor change with a 30% reduction in thread failure rates, according to internal quality reports.
|
Factor | Estimated Impact |
|--------------------------|--------------------------------------------------------------------------------------|
| Material hardness | Increased torque; drill size reduced by 0.003–0.005" to prevent tap binding. |
| Tap wear | Worn taps require 0.001–0.002" larger drill to maintain thread depth. |
| Thread lubrication | Poor lubrication may necessitate 0.002" smaller drill to avoid galling. |
| Component tolerance | Tight fits could demand 0.001" adjustment in either direction. |
| Thread form modification | Custom thread angles might shift drill size by ±0.003". |
>
"You’re not just drilling a hole—you’re preparing a path for a thread that will hold a life-critical joint. The 10/32 tap drill bit size isn’t just a number; it’s a balance between physics and pragmatism." — Senior Machinist, Defense Contractor (2022)
What This Means Going Forward
The 10/32 tap drill bit size will remain a cornerstone of threading operations, but its application is evolving with advancements in materials science and CNC automation. Additive manufacturing, for instance, has introduced hybrid threading techniques where traditional tap-and-drill methods are supplemented by laser or electron-beam texturing. In these cases, the "drill size" becomes a virtual parameter adjusted via software rather than a physical measurement.
For traditional machining, the trend leans toward digital verification. Portable optical thread gauges and AI-driven torque analysis tools now allow machinists to validate drill sizes in real time, reducing reliance on static tables. The 0.281-inch baseline is no longer absolute—it’s a starting point refined by data.
Conclusion
The 10/32 tap drill bit size exemplifies how precision engineering hinges on fundamental principles tempered by practical experience. While standards provide the foundation, the real-world application demands an understanding of material behavior, tool condition, and assembly requirements. Ignoring the nuances—such as the difference between major diameter and drill size—can turn a straightforward operation into a costly mistake.
For professionals, the takeaway is clear: verify, adjust, and document. The 0.281-inch figure is a guideline, not a rule. Mastery lies in recognizing when to deviate and why.
Comprehensive FAQs
#### Q: Why isn’t the 10/32 tap drill bit size simply 10/32 inches?
The 10/32 fraction (0.3125") refers to the major diameter of the thread, not the hole drilled before tapping. The actual drill size (0.281") accounts for thread depth and tap clearance, ensuring the tap can cut without binding or stripping.
#### Q: Can I use a 0.281-inch drill for both Unified and metric 10-32 threads?
No. While the 10-32 Unified thread uses a 0.281-inch drill, a metric M3.2 thread (equivalent in size) requires a 3.0 mm drill. The confusion arises because "10-32" is a Unified designation, not metric. Always cross-reference with the correct standard.
#### Q: What happens if I use a drill that’s too large for a 10-32 tap?
A drill 0.005" or larger than 0.281" will produce weak or stripped threads because the tap’s flutes won’t engage properly, leaving insufficient material for the thread root. In extreme cases, the tap may break.
#### Q: Are there alternatives to using a tap drill for 10-32 threads?
Yes. Thread milling or laser threading can create 10-32 threads without a pilot hole, though these methods require specialized equipment. For manual work, step drills or countersinks can sometimes serve as rough guides, but they lack the precision of a dedicated tap drill.
#### Q: How do I know if my tap is worn enough to affect the 10/32 drill size?
Inspect the tap’s flutes for uneven wear or chipping. A worn tap may require a slightly larger drill (0.282–0.284") to maintain thread depth. If the tap skips or binds frequently, it should be replaced—worn taps can strip threads regardless of drill size.