The Complete Overview of Rifled Barrel Manufacturing
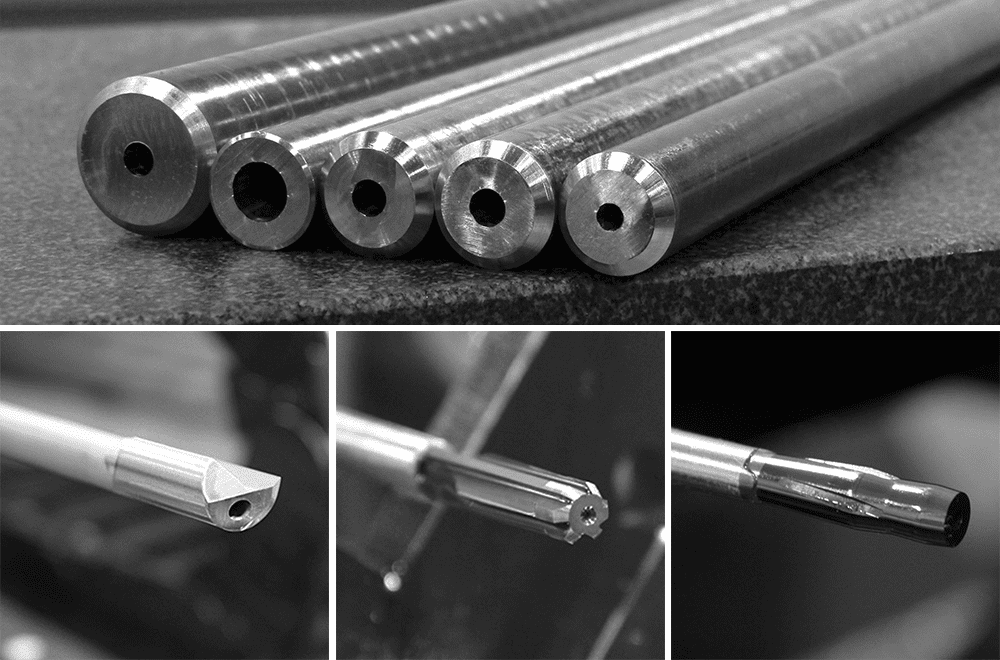
The stage of making rifled barrels when there is a creation of the land and grooves is often misunderstood as a singular step in gunmaking, but it’s actually a multi-phase operation where material science, thermal dynamics, and machining tolerances collide. At its core, rifling serves one purpose: to impart spin to a bullet, stabilizing its flight and eliminating the chaotic tumbling that plagues smoothbore projectiles. The lands (the raised portions between grooves) and grooves themselves are not arbitrary; their dimensions are calculated based on the bullet’s diameter, weight, and intended velocity. A 6mm Creedmoor barrel, for example, might feature a 1:7 twist rate, meaning the rifling completes one full rotation every seven inches of barrel length—a specification that’s the result of decades of empirical testing and computational ballistics. The process begins with a solid billet of steel, typically forged or cold-drawn to eliminate internal stresses. Before rifling, the barrel undergoes pre-machining, where the outer diameter is turned down to specification, and the bore is roughly drilled to near-final dimensions. This is where the first critical decisions are made: will the rifling be cut (as in traditional broaching) or hammered (as in button rifling)? Cut rifling uses a tool with teeth that remove material, creating sharp edges that can accelerate wear. Hammered rifling, by contrast, uses a hardened mandrel to cold-flow the metal, producing smoother surfaces and better longevity—though it requires higher forces and precise material properties. The choice isn’t just about method; it’s about the stage of making rifled barrels when there is a creation of the land and grooves, where the interaction between tool and metal determines whether the rifling will hold up after thousands of rounds.Historical Background and Evolution
The concept of rifling dates back to the 15th century, when German and Austrian gunsmiths experimented with twisted grooves to improve accuracy. However, it wasn’t until the early 1800s that rifling became practical for military use, thanks to advancements in metallurgy and machining. The stage of making rifled barrels when there is a creation of the land and grooves was revolutionized by the Springfield Armory in the 1840s, which adopted a standardized rifling process for the M1842 rifle. This rifle used a three-groove rifling pattern, a design that became a cornerstone of American firearms engineering. The transition from smoothbore muskets to rifled barrels wasn’t just a technological leap—it was a tactical one, as rifled weapons could penetrate armor and achieve ranges previously unimaginable. The 20th century brought further refinements, with the introduction of button rifling in the 1930s, pioneered by Jan Kynčl of Czechoslovakia. This method used a hardened steel button pressed through the bore, cold-hammering the metal to create rifling without removing material—a technique that became standard for high-end rifles like the CZ 550. Meanwhile, the rise of automatic weapons demanded faster production methods, leading to the dominance of broaching machines in military arsenals. Today, the stage of making rifled barrels when there is a creation of the land and grooves is often handled by CNC lathes equipped with live-tooling capabilities, allowing for real-time adjustments to rifling profiles. Even so, traditional methods persist in niche applications, such as hand-lapped rifling for match-grade barrels, where human precision still outpaces machines in certain contexts.Core Mechanisms: How It Works
The mechanics of rifling creation hinge on three variables: toolpath, material deformation, and heat management. In cut rifling, a broach or single-point tool removes material in a controlled manner, carving the grooves while leaving the lands as sharp ridges. The depth of the grooves is typically 0.005 to 0.015 inches, depending on the caliber, and the twist rate (measured in inches per revolution) is calculated to match the bullet’s length and weight. For example, a 6.5 Creedmoor might use a 1:8 twist, while a .308 Winchester often employs a 1:10 or 1:12 twist to stabilize heavier projectiles. The stage of making rifled barrels when there is a creation of the land and grooves also involves lead-in and lead-out tapers, where the rifling gradually deepens and then shallows to prevent bullet deformation during engagement. Hammered rifling, by contrast, relies on plastic deformation rather than material removal. A hardened steel button—often with a polygonal or hexagonal cross-section—is forced through the bore at high pressure, causing the metal to flow and conform to the button’s shape. This method produces smoother surfaces with fewer stress risers, reducing the risk of barrel fatigue over time. The trade-off is higher initial cost and the need for high-quality steel that can withstand the compressive forces. Modern CNC rifling combines elements of both approaches, using ball-nose end mills or fly-cutting tools to achieve precise, repeatable results. Some advanced systems even incorporate laser-assisted machining, where a laser pre-heats the metal to improve chip evacuation and surface finish.Key Benefits and Crucial Impact
The stage of making rifled barrels when there is a creation of the land and grooves isn’t just a manufacturing step—it’s the linchpin of a rifle’s performance. A well-executed rifling job ensures consistent bullet spin, which translates to tighter groupings and longer effective ranges. For competitive shooters, this difference can mean the gap between a sub-MOA rifle and one that struggles to hold 1.5 inches at 100 yards. In military applications, precise rifling is critical for penetration and terminal ballistics, where a poorly rifled barrel can fail to stabilize a bullet, reducing lethality. Even in budget firearms, the geometry of the rifling affects fouling and barrel life, as sharp edges accelerate lead buildup and erosion. The impact extends beyond accuracy. The stage of making rifled barrels when there is a creation of the land and grooves also influences barrel longevity. Poorly executed rifling can lead to stress concentrations, causing cracks or splits after prolonged use. Conversely, hammered rifling or polygonal rifling reduces fouling, extending the life of the barrel and improving reliability in high-volume applications. For collectors and enthusiasts, the rifling profile can even serve as a signature of a rifle’s origin—whether it’s the six-groove pattern of a Remington 700 or the five-groove twist of a Savage Model 110."Rifling isn’t just about spin—it’s about the marriage of metal and motion. Get it wrong, and you’re not just building a gun; you’re building a liability." — John Taylor, former chief ballistician at Hornady Manufacturing
Major Advantages
- Improved accuracy: Proper rifling ensures consistent bullet spin, reducing dispersion and improving shot grouping.
- Extended barrel life: Smoother rifling profiles (e.g., hammered or polygonal) reduce fouling and stress-related failures.
- Enhanced penetration: Tighter rifling tolerances allow for better bullet stabilization, improving terminal performance.
- Versatility in caliber: Adjustable rifling profiles enable the same barrel to chamber multiple calibers (e.g., a .243 Win barrel that can also shoot .223 Rem).
- Reduced recoil and muzzle rise: Optimized rifling can improve bullet efficiency, slightly mitigating felt recoil in high-power rifles.
Comparative Analysis
| Method | Advantages |
|---|---|
| Broaching | Fast, cost-effective for mass production; suitable for soft steel alloys. |
| Button Rifling | Smoother surfaces, longer barrel life; preferred for high-end rifles. |
| CNC Milling | High precision, customizable rifling profiles; ideal for experimental designs. |
Future Trends and Innovations
The stage of making rifled barrels when there is a creation of the land and grooves is evolving with additive manufacturing and smart materials. Companies like RUAG and BAE Systems are experimenting with 3D-printed rifling, where selective laser melting (SLM) creates internal structures impossible with traditional machining. This could lead to barrels with variable twist rates or integrated cooling channels to reduce thermal expansion. Meanwhile, nanostructured coatings—such as diamond-like carbon (DLC)—are being tested to improve rifling durability and reduce friction. Another frontier is adaptive rifling, where sensors monitor barrel wear in real-time and adjust rifling profiles via electrochemical machining to maintain performance. Looking ahead, the stage of making rifled barrels when there is a creation of the land and grooves may also incorporate AI-driven optimization. Machine learning algorithms could analyze thousands of shooting scenarios to recommend optimal rifling geometries for specific bullet types, eliminating the guesswork that currently plagues custom barrel builds. For now, however, the craft remains a blend of tradition and innovation, where the human touch—whether in hand-lapping a match-grade barrel or fine-tuning a CNC program—still holds sway over the final result.
Conclusion
The stage of making rifled barrels when there is a creation of the land and grooves is more than a manufacturing process; it’s the foundation of ballistic science. From the hand-cut rifling of 19th-century muskets to the CNC-precision barrels of today, each advancement has pushed the boundaries of what a rifle can achieve. The choice of method—whether broaching, button rifling, or laser-assisted machining—isn’t just about efficiency; it’s about balancing performance, durability, and cost. As materials and technologies evolve, so too will the stage of making rifled barrels when there is a creation of the land and grooves, but the core principle remains unchanged: precision in the rifling means precision in the shot. For shooters, this means better accuracy, longer barrel life, and greater reliability. For engineers, it’s a challenge to innovate without sacrificing the fundamentals. And for historians, it’s a testament to the enduring marriage of craftsmanship and science that defines firearms engineering.Comprehensive FAQs
Q: Can rifling be repaired if damaged?
A: In most cases, no. Rifling damage—such as groove wear or lands collapsing—cannot be fully restored without re-cutting the entire bore. Some gunsmiths may attempt to re-profile the rifling using specialized tools, but this is rare and often ineffective for heavily worn barrels. Replacement is the only reliable solution.
Q: How does rifling affect bullet selection?
A: Rifling twist rate and groove depth dictate which bullets will stabilize properly. For example, a 1:7 twist is ideal for light, fast bullets (e.g., 6mm Creedmoor), while a 1:12 twist works better for heavy, long bullets (e.g., .308 Winchester). Using a bullet that’s too long or too short for the rifling can result in poor stabilization, increased wear, or even bullet failure.
Q: Is polygonal rifling better than traditional rifling?
A: Polygonal rifling (e.g., hexagonal or octagonal profiles) reduces fouling and improves velocity slightly, but it’s not universally "better." Traditional rifling remains more common because it’s cheaper to produce and easier to maintain. Polygonal rifling excels in high-volume applications (e.g., military rifles) where fouling is a critical concern.
Q: How often should rifling be inspected?
A: Rifling should be inspected annually for competitive shooters and every 5,000–10,000 rounds for recreational use. Signs of wear include increased bullet deformation, reduced accuracy, or visible lead buildup in the grooves. A bore scope is the best tool for this inspection, allowing the shooter to verify rifling integrity without disassembling the barrel.
Q: Can a smoothbore barrel be converted to rifled?
A: Technically possible, but not practical for most applications. Converting a smoothbore requires re-drilling the bore and re-cutting rifling, which weakens the barrel and often reduces its structural integrity. The process is expensive, time-consuming, and rarely results in performance comparable to a factory rifled barrel. It’s generally better to replace the barrel if rifling is desired.
