Where It All Began
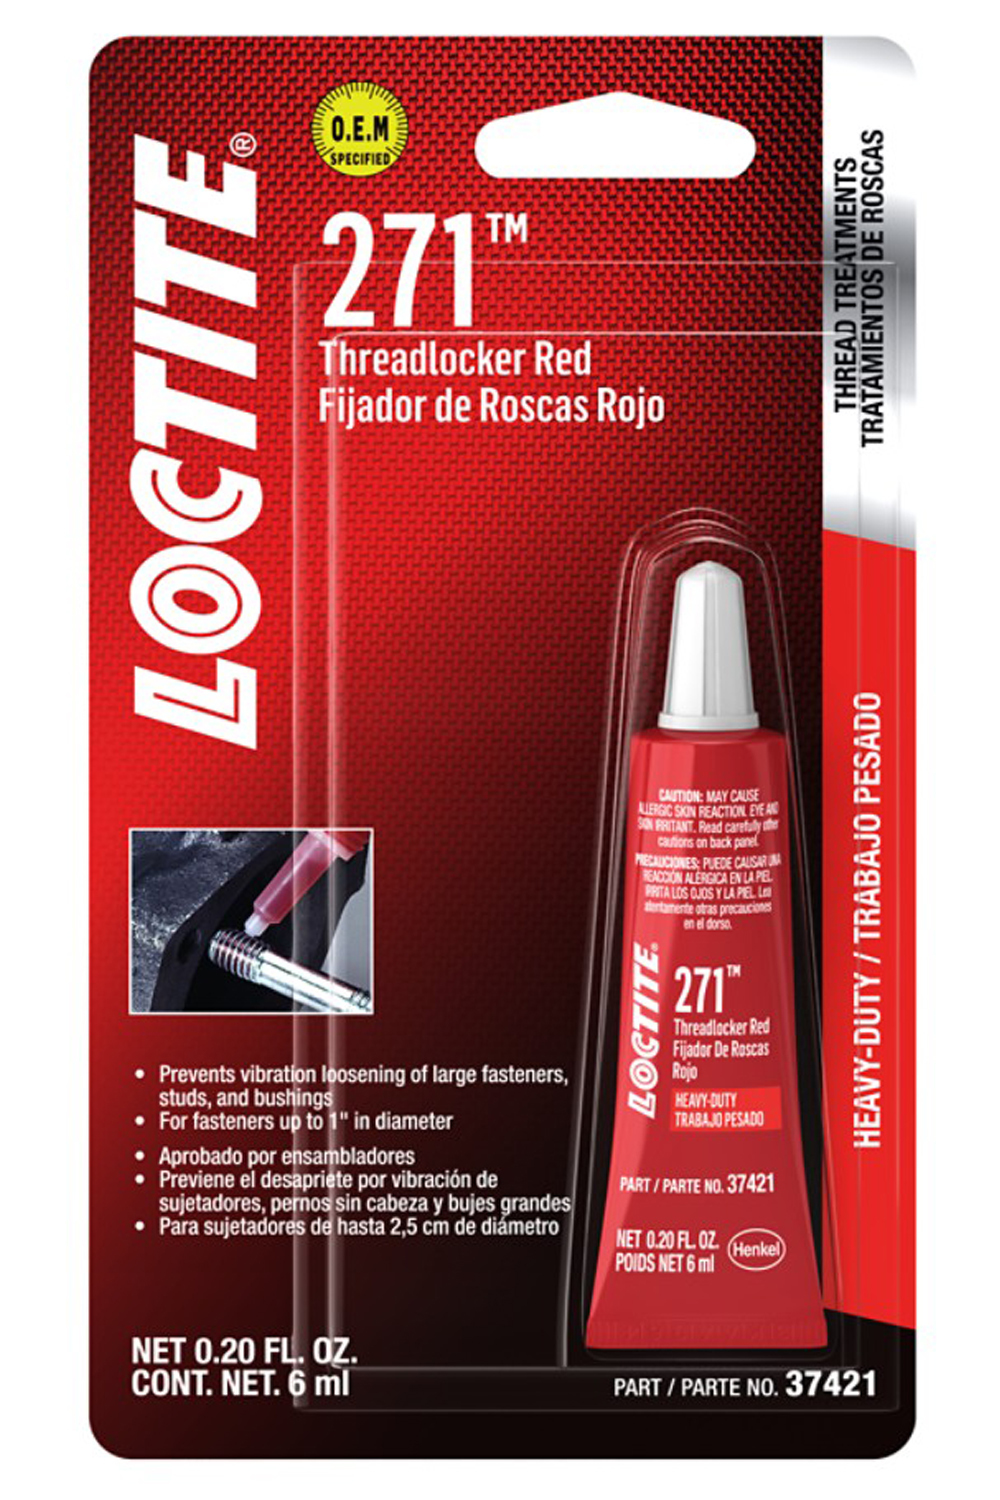
The origins of red threadlocker vs blue trace back to the 1960s, when Loctite—then a small adhesives company—began experimenting with anaerobic sealants. These compounds cured only when deprived of oxygen, making them perfect for locking threaded fasteners. The first commercial product, a straw-colored liquid, was marketed as a "threadlocker" for precision machinery. It wasn’t red or blue yet, but the foundation was laid: a material that could transform from liquid to solid under the right conditions. The color coding emerged in the 1970s as Loctite expanded its product line. Blue threadlocker (Loctite 271) was formulated for medium-strength applications, balancing cost and performance. It became the workhorse of factories, where most fasteners didn’t face extreme stress. Red threadlocker (Loctite 243), introduced later, was engineered for high-vibration and high-temperature environments—think aircraft engines or heavy-duty truck transmissions. The colors weren’t arbitrary; they signaled red threadlocker vs blue as a spectrum of reliability.The Early Signs
By the late 1970s, the split was evident in industry manuals. Blue threadlocker dominated in automotive assembly, where most fasteners saw moderate stress. Red made appearances in niche applications, but its higher price tag limited adoption. The turning point came when a major aerospace contractor mandated red for critical components, citing field failures with blue. The incident wasn’t publicized, but it forced manufacturers to reconsider: was blue threadlocker’s reputation as the "safe choice" actually a liability in high-stakes environments? The divide deepened as threadlocker technology advanced. Blue remained the go-to for general use, while red became synonymous with mission-critical applications. The colors weren’t just marketing—they were a shorthand for risk tolerance. A factory worker applying blue might not think twice; an engineer specifying red knew the stakes.The Turning Point
The late 1980s marked the moment red threadlocker vs blue stopped being a technical debate and became an industrial philosophy. A series of high-profile fastener failures in automotive and aerospace sectors exposed blue’s limitations under thermal cycling. Red, though more expensive, offered a margin of safety that blue couldn’t match. The shift wasn’t immediate—old habits die hard—but the writing was on the wall. The tipping point arrived in 1991, when a major aircraft manufacturer published internal data showing that red threadlocker reduced fastener loosening by 60% in extreme conditions. The report wasn’t widely shared, but it changed procurement policies overnight. Suddenly, red wasn’t just an option; it was the default for anything beyond routine assembly."You don’t use blue when the alternative is a multimillion-dollar recall. That’s the moment the industry realized red wasn’t a luxury—it was insurance." — Former Loctite R&D Engineer (anonymous, 1993)The backlash was predictable. Blue threadlocker’s advocates argued that red’s higher viscosity could cause over-torquing or improper sealing. But the data spoke louder. By 1995, red had carved out a permanent niche in high-reliability sectors, while blue remained entrenched in cost-sensitive applications.
The Build-Up, Year by Year
| Period | Key Developments |
|---|---|
| 1960s–1970s | Loctite introduces anaerobic sealants. Blue threadlocker (Loctite 271) becomes the standard for general use. Red (Loctite 243) is developed for high-stress applications but remains niche. |
| 1980s | Aerospace and automotive sectors begin mandating red for critical components. Field failures with blue in high-vibration environments drive adoption shifts. |
| 1990s–Present | Red threadlocker dominates in aerospace, heavy machinery, and medical devices. Blue remains prevalent in automotive assembly, consumer goods, and low-risk applications. Competitors (Permatex, Permabond) introduce similar color-coded systems. |
Lessons From the Journey
- Color as shorthand: The red vs. blue distinction became a proxy for risk assessment—no training required. Workers learned to associate colors with performance expectations.
- Cost vs. reliability tradeoff: Blue’s affordability made it indispensable in high-volume manufacturing, while red’s premium pricing limited its use to high-stakes applications.
- Industry fragmentation: Aerospace and medical sectors embraced red early, while automotive lagged due to legacy systems and cost constraints.
- Regulatory influence: Aviation standards (e.g., FAA guidelines) explicitly favored red for critical fasteners, accelerating its adoption in other high-reliability fields.
- The myth of "one-size-fits-all": Blue threadlocker’s failures in extreme conditions proved that red threadlocker vs blue wasn’t just preference—it was a question of engineering judgment.
Where Things Stand Today
Today, red threadlocker vs blue is less about rivalry and more about specialization. Red dominates in sectors where failure is unacceptable: aerospace, medical implants, and heavy industrial machinery. Blue persists in automotive assembly, consumer electronics, and applications where cost efficiency outweighs performance margins. The lines have blurred slightly—some hybrid formulations now bridge the gap—but the color coding remains a cultural touchstone. What’s changed is the conversation. No longer is the debate framed as "red vs. blue" but as "which is right for this application?" Engineers now consider viscosity, thermal stability, and chemical compatibility before reaching for a color. Yet, in the trenches, old habits linger. A mechanic might default to blue for a routine engine rebuild, while an aerospace technician treats red like a sacred ritual.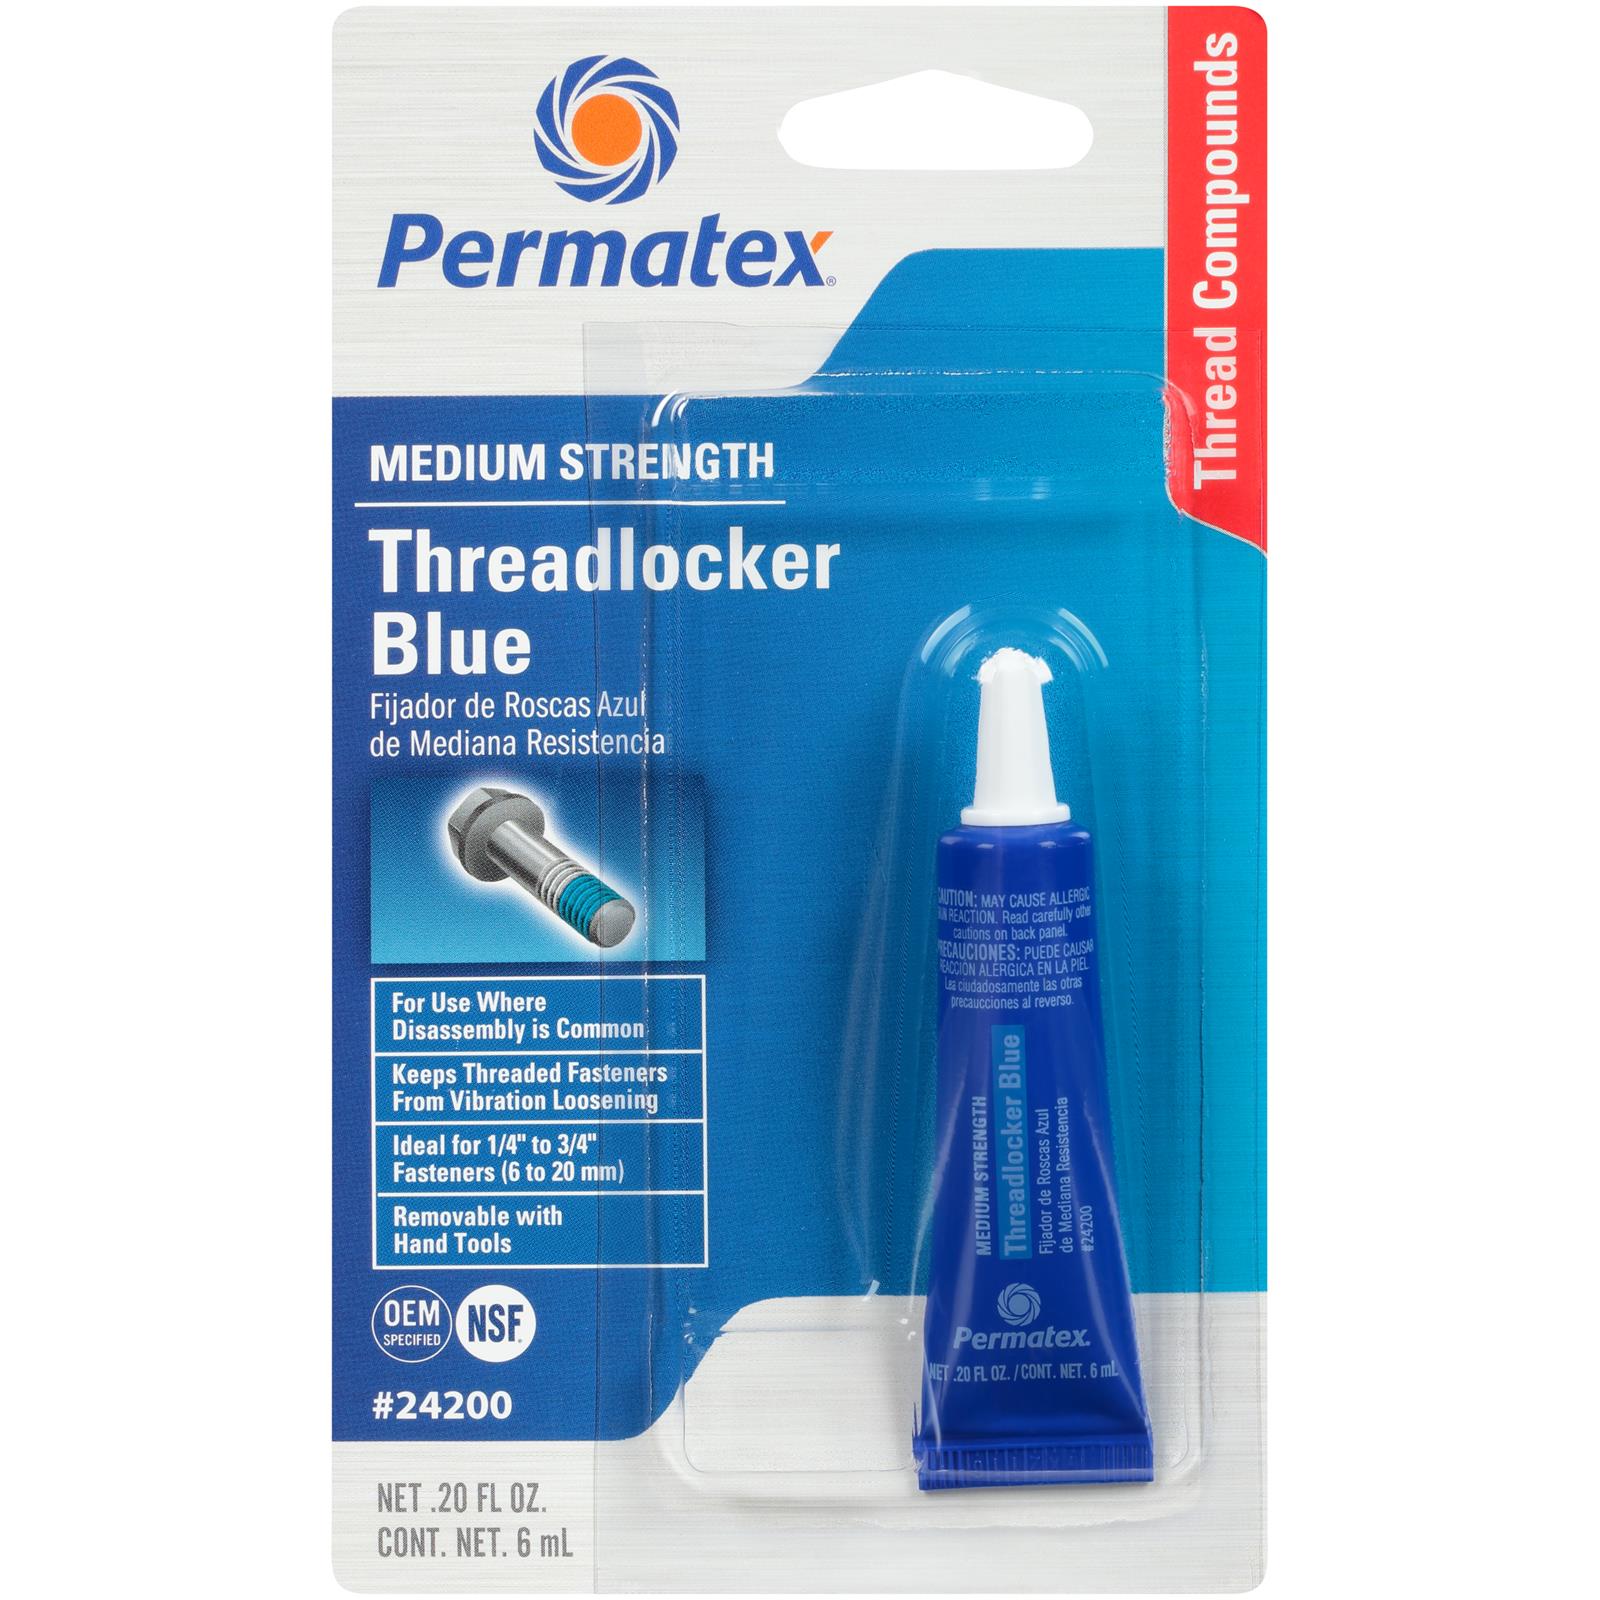
Conclusion
The story of red threadlocker vs blue is more than a chemical showdown—it’s a case study in how industries balance risk and economics. Blue’s versatility made it a manufacturing staple, while red’s aggressiveness redefined safety in high-stakes environments. The rivalry wasn’t about superiority; it was about context. One color couldn’t do everything, and the market adapted accordingly. As threadlocker technology evolves—with smart adhesives and self-healing polymers on the horizon—the color divide may fade. But the principles remain: understanding the environment, anticipating failure, and choosing the right tool for the job. In that sense, the debate over red and blue was never just about adhesives. It was about how industries learn to trust—or distrust—their own assumptions.Comprehensive FAQs
Q: Can I use red threadlocker instead of blue in general applications?
Technically yes, but it’s often overkill. Red threadlocker’s higher viscosity and strength are unnecessary for low-stress fasteners, risking over-torquing or improper sealing. Blue is designed for these scenarios and is more cost-effective.
Q: Why does red threadlocker cost more than blue?
The higher price reflects its formulation: red contains more aggressive anaerobic polymers and additives for thermal stability, making it suitable for extreme conditions. Blue uses a simpler, less expensive chemical profile optimized for moderate stress.
Q: Are there alternatives to red and blue threadlocker?
Yes. Competitors like Permatex (Thread Lock Blue/Red) and Permabond offer similar color-coded systems. Some hybrid products blend properties of both, but color coding remains a standard reference in many industries.
Q: Does temperature affect the choice between red and blue?
Absolutely. Blue threadlocker struggles in high-temperature environments (above 120°C/248°F), where it may degrade or lose grip. Red is formulated to withstand temperatures up to 260°C (500°F), making it essential for engines, exhaust systems, and industrial machinery.
Q: Is red threadlocker safe for aluminum fasteners?
Both red and blue can be used with aluminum, but red’s higher clamping force requires caution. Aluminum’s lower tensile strength means over-tightening with red can strip threads or damage the material. Always follow manufacturer torque specs.
Q: How do I know if my application needs red vs. blue?
Ask these questions:
- Will the fastener experience high vibration or thermal cycling? → Red.
- Is this a low-stress, cost-sensitive application? → Blue.
- Are safety or regulatory standards involved (e.g., aerospace, medical)? → Red is often mandatory.
- Do you need ease of disassembly? → Blue (red’s bond is harder to break).
Q: Can I mix red and blue threadlocker?
No. Mixing them can compromise performance—red’s aggressive chemistry may interfere with blue’s curing process, leading to weak bonds or improper sealing. Use them as specified for their intended applications.
