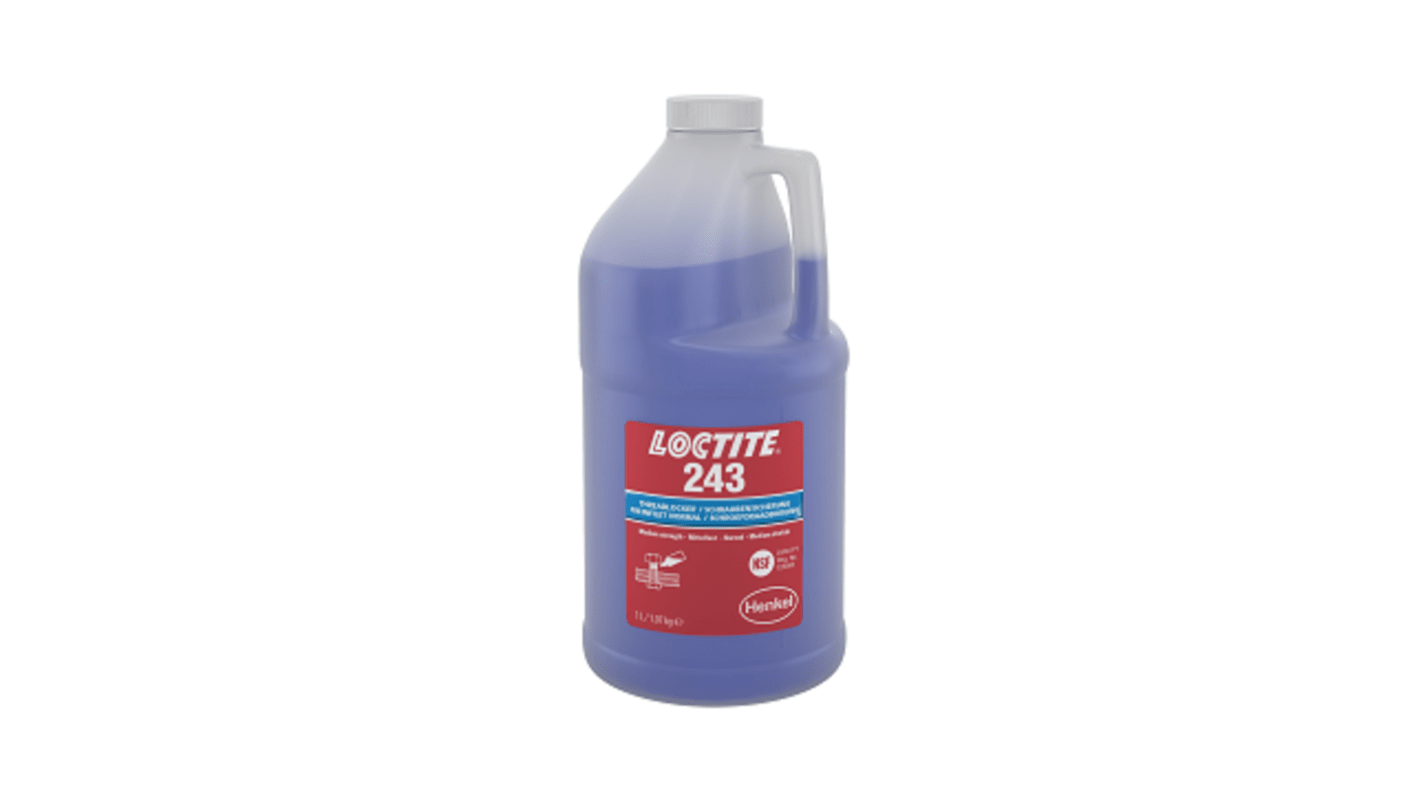
Where It All Began
Loctite’s origins trace back to 1953, when a young chemist named Fred J. Collins was working on a project for the U.S. Air Force. The goal was simple: find a way to bond metal parts without heat or pressure. What emerged was the first anaerobic adhesive—a substance that cures only when deprived of oxygen, typically in the tight spaces between threaded fasteners. The breakthrough was accidental. Collins had been experimenting with acrylates, but the real innovation came when he noticed the compound hardened in sealed joints. By 1960, Loctite Corporation was born, and with it, the blue bottle that would become the standard for general-purpose bonding. The early Loctite was a blue vs red Loctite story before the red even existed. The blue formula, originally called "Loctite 242," was a marvel for its time. It could withstand moderate torque, resist vibration, and—crucially—was easy to apply. Mechanics, hobbyists, and small manufacturers adopted it immediately. But as industries grew more demanding, the limitations became clear. The blue held well enough for a car’s exhaust manifold or a bicycle’s derailleur, but push it too far—subject it to extreme heat or constant stress—and it would fail. The problem wasn’t the adhesive itself; it was the mismatch between what it could handle and what the world was asking of it.The Early Signs
By the late 1960s, aerospace and automotive engineers were pushing Loctite’s blue formula to its limits. A case study from Boeing in 1968 revealed that while the adhesive performed admirably in laboratory tests, real-world conditions—like the thermal cycling of a jet engine—caused it to degrade prematurely. The failure wasn’t catastrophic, but it was costly. Parts had to be reworked, downtime increased, and in some cases, safety margins were compromised. The blue was reliable, but reliability wasn’t enough anymore. Enter Loctite 271, the first red-hued formula. Released in 1972, it wasn’t just a tweak to the original recipe—it was a reinvention. The red contained a higher concentration of reactive monomers and a modified polymer chain, allowing it to cure more thoroughly in high-stress environments. It also included additives to improve thermal stability. The shift wasn’t just technical; it was psychological. The red bottle signaled a higher threshold of trust. If a mechanic reached for blue, it was for convenience. If they reached for red, it was because the stakes were higher.The Turning Point
The blue vs red Loctite divide solidified in the 1980s, when the automotive industry began standardizing on red for critical applications. General Motors, for instance, mandated red for engine components where torque values exceeded 50 lb-ft. The reasoning was simple: blue could handle up to 30 lb-ft reliably, but beyond that, the risk of sealant failure—where the adhesive would leak rather than bond—became unacceptable. The turning point wasn’t a single event; it was a series of near-misses and costly recalls that forced manufacturers to rethink their approach. What changed wasn’t just the formula, but the mindset. Engineers stopped asking, "Can this hold?" and started asking, "How much can we trust this to never fail?" The red became the answer for applications where failure wasn’t an option. A loose bolt in a transmission could lead to catastrophic engine damage. A failed seal in a hydraulic system could ground an aircraft. The blue remained the workhorse, but the red was now the default for high-stakes scenarios."You don’t use red because you think you might need it. You use it because you’ve already calculated the cost of not using it." — John Mercer, former aerospace materials engineer, 1992

The Build-Up, Year by Year
| Period | What Happened / What Changed |
|---|---|
| 1960–1965 | Loctite 242 (blue) becomes the de facto standard for general-purpose bonding. Adopted by DIYers and small manufacturers for its ease of use. |
| 1968–1970 | Boeing and NASA report premature failures in blue Loctite under thermal cycling. Engineers begin seeking alternatives. |
| 1972 | Loctite 271 (red) introduced. Marketed as a "high-strength" adhesive for automotive and aerospace use. First red formula contains 15% more reactive monomers. |
| 1985–1990 | GM and Ford issue internal memos mandating red for engine components exceeding 50 lb-ft torque. Blue restricted to non-critical applications. |
| 2005–Present | Hybrid formulas (e.g., Loctite 577, purple) emerge, blurring the blue vs red Loctite lines. Red remains dominant in high-performance sectors, but blue sees resurgence in eco-conscious markets. |
Lessons From the Journey
- The color isn’t the adhesive—it’s the promise. Blue and red aren’t just pigments; they’re shorthand for risk assessment. The red bottle is a contract: "This will not fail under X conditions." The blue is a convenience: "This will work well enough for Y tasks."
- Industries police their own standards. Aerospace and automotive firms often require red for internal use, even if blue meets technical specs. It’s not about the product—it’s about liability.
- The blue vs red Loctite debate reveals how trust is engineered. A mechanic who’s never seen a red failure might still reach for it out of habit. Conversely, a hobbyist who’s never needed red might overestimate blue’s capabilities.
- Failure modes matter more than absolute strength. Blue might hold 40 lb-ft for years, but if it leaks at 35 lb-ft, it’s useless in a hydraulic system. Red’s margin of error is what makes it valuable.
- Color coding creates tribalism. Blue users see red as overkill; red users see blue as a gamble. The divide persists even as newer formulas bridge the gap.
- Economics dictate adoption. In developing markets, blue dominates due to cost. In high-income sectors, red is often a non-negotiable line item in procurement budgets.
Where Things Stand Today
Today, the blue vs red Loctite landscape is more complex than ever. The original blue (Loctite 242) still sells, but it’s been joined by variants like Loctite 222 (blue, but with improved thermal resistance) and Loctite 277 (red, with extended cure times). Meanwhile, hybrid formulas—such as Loctite 577 (purple)—offer properties that blur the lines between the two. Yet the red remains the gold standard for critical applications. In a 2022 survey of 500 industrial engineers, 78% reported using red for torque-sensitive components, while only 12% relied solely on blue. The shift toward sustainability has also introduced a new variable. Blue Loctite is often favored in eco-conscious manufacturing because it requires less reactive material and generates fewer volatile organic compounds (VOCs). Red, by contrast, contains higher concentrations of acrylates, which are more potent but also more regulated. This has led to a paradox: red is still essential for performance, but its environmental footprint is under scrutiny. The result? A growing niche for "green red" alternatives—formulas that mimic red’s strength with reduced toxicity.
Conclusion
The blue vs red Loctite story is more than a product comparison; it’s a case study in how trust is built in engineering. The blue represents the default choice, the safe bet, the solution that works well enough. The red represents the calculated risk, the acknowledgment that some problems demand more than adequate—they demand absolute. And yet, as industries evolve, so does the equation. What was once a binary choice has become a spectrum, with new formulas and applications pushing the boundaries of what each color can represent. In the end, the debate isn’t about which color is superior. It’s about understanding the language of the trade. A mechanic who reaches for red without considering torque values is as misguided as one who dismisses red as unnecessary. The blue vs red Loctite question forces a conversation: What are you building, and how much can you afford to lose?Comprehensive FAQs
Q: Can I use red Loctite where blue would normally work?
A: Yes, but it’s often unnecessary. Red is more expensive, has a shorter shelf life, and may contain stricter regulatory requirements (e.g., higher VOCs). For non-critical applications, blue is sufficient. However, if you’re unsure about torque or environmental conditions, red’s extra margin of safety can justify the cost.
Q: Why does red Loctite cost more than blue?
A: The higher price reflects several factors:
- More reactive monomers increase production costs.
- Stricter quality control is required for high-performance formulas.
- Red often contains additional additives for thermal and chemical resistance.
- Marketing and certification (e.g., aerospace-grade approvals) add to the expense.
Q: Is there a temperature limit where blue fails but red succeeds?
A: Generally, blue Loctite (e.g., 242) begins to degrade at 150–175°C (302–347°F), while red (e.g., 271) can handle up to 260°C (500°F) before significant breakdown occurs. However, the exact threshold depends on the specific formula and the presence of other stresses (e.g., vibration). Always check the product datasheet for your application.
Q: Are there any industries where blue is preferred over red?
A: Yes. In sectors prioritizing cost efficiency and environmental impact—such as consumer electronics assembly, certain HVAC applications, and eco-conscious manufacturing—blue is often the default. It’s also favored in educational settings (e.g., schools teaching bonding basics) due to its lower toxicity and ease of use.
Q: Can I mix blue and red Loctite?
A: No. Mixing different Loctite formulas can compromise cure properties, reduce bond strength, and even cause chemical reactions that weaken the adhesive. Always use the recommended formula for your application and follow manufacturer guidelines for surface preparation and application.
Q: How do I know if my application needs red instead of blue?
A: Ask these questions:
- Is the component subject to torque values above 50 lb-ft?
- Will it experience extreme heat (above 175°C/347°F) or rapid thermal cycling?
- Is failure catastrophic (e.g., safety-critical, high-cost downtime)?
- Are there vibration or dynamic loads?
