
Breaking Down the Numbers
Dial indicators measure displacement with resolutions as fine as 0.0001 inches (0.0025 mm). Their accuracy hinges on three variables: the magnification ratio of the gear train, the dial face’s least count, and the mechanical play in the spindle. A typical 0–1-inch indicator with a 10:1 ratio will show 0.001-inch increments per division, but internal friction can introduce errors up to ±0.0005 inches if not properly maintained. Industry benchmarks suggest that how to use dial indicators effectively reduces measurement uncertainty by 60–80% compared to uncalibrated setups, though this depends on the operator’s skill. The cost of misapplication is tangible. In automotive manufacturing, a single misaligned indicator during cylinder bore gauging can lead to piston-to-wall clearances outside specification, forcing costly rework. Similarly, aerospace components with tolerances of ±0.005 mm demand indicators calibrated to NIST traceable standards—a process that adds $200–$500 per tool if outsourced. The trade-off between speed and precision is real: rushing through how to use dial indicators can turn a $50 gauge into a liability.The Verified Baseline
Every dial indicator requires a stable reference surface. Surface plates certified to Grade AA (flatness within 0.0002 inches per 12 inches) are the gold standard for calibration. Before use, inspect the indicator’s contact tip for wear—even a 0.0005-inch radius difference can skew readings. Zero the dial by gently lowering the spindle onto the reference surface, then adjusting the bezel until the needle aligns with the zero mark. This step is non-negotiable; skipping it introduces systematic error that compounds with each measurement. The magnification mechanism—typically a 10:1 or 20:1 gear ratio—converts spindle movement into dial rotation. A 0.001-inch spindle movement on a 10:1 indicator will move the needle one full division. However, backlash in the gears (often 0.0002–0.0005 inches) means readings taken in opposite directions may vary. To mitigate this, always approach measurements from the same direction, or use a reversing lever if available.What the Estimates Suggest
Industry estimates place the average operator error at how to use dial indicators around 20–30% of the tool’s least count due to parallax, improper contact force, or environmental shifts. Temperature fluctuations of just 10°F (5.5°C) can cause a 1-inch aluminum part to expand by 0.0006 inches, throwing off readings if unaccounted for. Some machinists compensate by storing indicators in climate-controlled cabinets, though this adds $1,500–$3,000 to setup costs for high-volume operations. For applications requiring sub-micron precision—such as semiconductor wafer inspection—digital dial indicators with electronic amplification are preferred. These eliminate gear backlash but cost five to ten times more than mechanical models. The choice often boils down to budget: mechanical indicators dominate in how to use dial indicators for general machining, while digital variants are reserved for R&D or medical device manufacturing where tolerances are tighter than human hair width.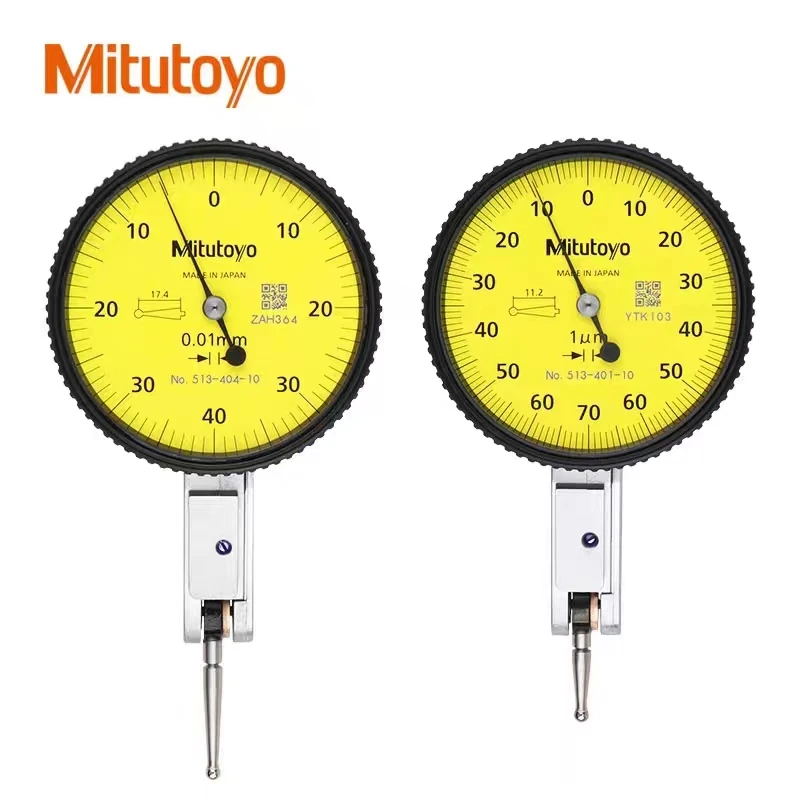
Case Study: A Closer Look
In 2019, a German automotive supplier faced a quality crisis when how to use dial indicators incorrectly during piston ring gap measurements led to 12,000 engines failing emissions tests. The root cause? Operators were zeroing the dial against the cylinder wall itself rather than a certified reference block, introducing a 0.0015-inch systematic offset. The fix required retraining workers and recalibrating 47 indicators—an investment of €85,000—but saved €2.1 million in warranty claims. The incident highlighted three critical factors in how to use dial indicators for internal measurements: 1. Reference stability: The cylinder wall’s own taper (often 0.0005 inches per inch) compounded the error. 2. Contact force consistency: Applying too much pressure could deform soft cast-iron surfaces. 3. Environmental control: The shop’s 75°F (24°C) temperature swings caused aluminum gauges to drift by 0.0003 inches over an 8-hour shift.“You can buy the most expensive indicator, but if the operator doesn’t understand the physics of the setup, it’s worthless. We now require a three-point calibration check before every production run.” — Head of Quality Control, Stuttgart Engine Works (anonymized)
| Factor | Estimated Impact on Measurement Error |
|---|---|
| Improper zeroing technique | ±0.001–0.003 inches (25–75 µm) |
| Temperature variation (10°F swing) | ±0.0005–0.001 inches (13–25 µm) |
| Gear backlash in 10:1 indicator | ±0.0002–0.0005 inches (5–13 µm) |
| Parallax error (misaligned viewing) | ±0.0005–0.002 inches (13–50 µm) |
What This Means Going Forward
The future of how to use dial indicators lies in hybrid systems. Many modern indicators now feature digital readouts with memory functions, allowing operators to log measurements directly to a shop floor database. This reduces human error by eliminating manual transcription and enables statistical process control (SPC) analysis. For example, a CNC lathe operator can now track spindle runout trends over time, predicting maintenance needs before parts fail. However, the core principles remain unchanged. Stability, calibration, and environmental control are non-negotiable. As tolerances shrink across industries—from 3D-printed medical implants to electric vehicle motor shafts—the demand for how to use dial indicators with sub-micron precision will grow. The tools themselves may evolve, but the operator’s understanding of leverage, friction, and reference frames will always dictate the outcome.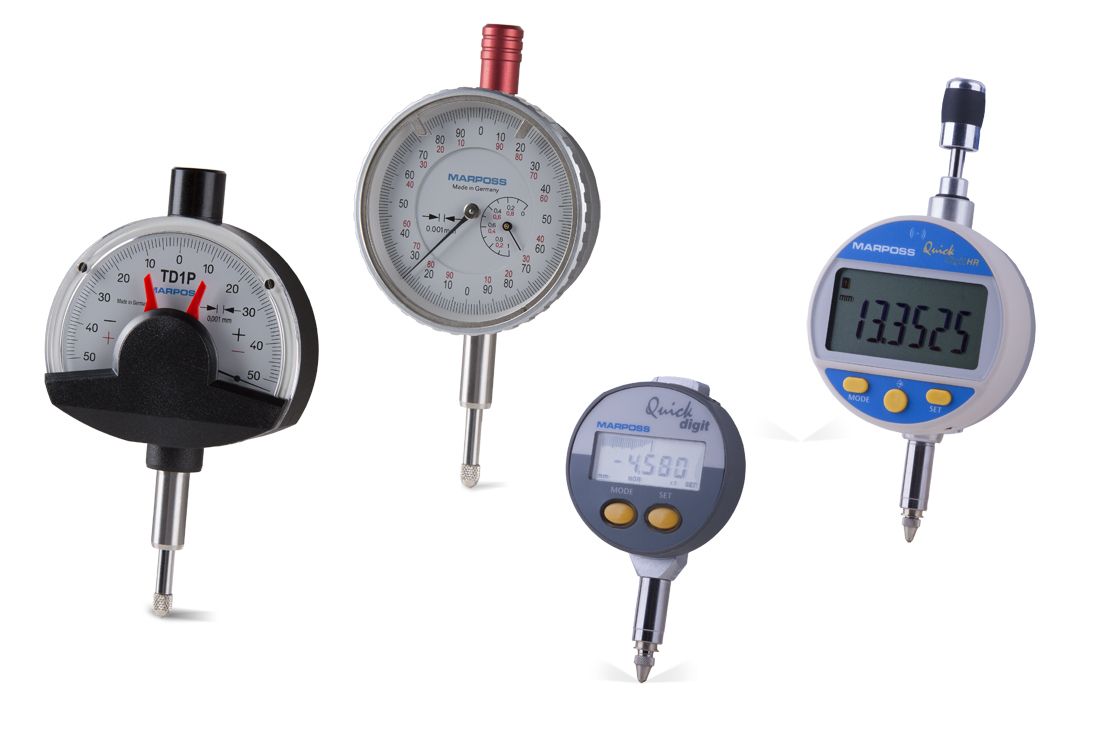
Conclusion
Dial indicators are not just tools; they are precision amplifiers that extend the operator’s ability to perceive the world at a microscopic scale. Mastering how to use dial indicators requires more than reading a manual—it demands an appreciation for the interplay between mechanics, materials, and environment. The best practitioners treat each measurement as an experiment, verifying assumptions against known standards. For hobbyists and professionals alike, the payoff is clear: how to use dial indicators correctly transforms a $100 tool into a $10,000 asset by catching defects before they become failures. The investment isn’t in the gauge itself, but in the discipline to wield it with precision.Comprehensive FAQs
Q: How often should I calibrate my dial indicator?
A: Mechanical indicators should be calibrated annually or after every 5,000 uses, whichever comes first. Digital models with built-in calibration routines may only require bi-annual checks. Always use a NIST-traceable gauge block set for verification—never rely on the indicator’s own zeroing function as a calibration reference.
Q: Can I use a dial indicator for angular measurements?
A: Yes, but only with an angular sine plate or tilting table. The indicator measures vertical displacement as the plate rotates, converting it to an angle via trigonometry. For example, a 0.001-inch rise over a 1-inch radius equals 0.0573 degrees of tilt. Without proper fixturing, parallax and contact point shifts will introduce errors.
Q: Why does my indicator’s reading jump when I press the spindle?
A: This is spindle compliance—the internal flex in the mechanism. High-quality indicators use preloaded ball bearings to minimize this, but excessive force (e.g., >0.5 lbs) will still cause deflection. For sensitive applications, use a lightweight contact tip (e.g., sapphire or ruby) and apply just enough pressure to maintain contact without bending the spindle.
Q: How do I check for backlash in my dial indicator?
A: Rotate the spindle clockwise until it bottoms out, then note the reading. Reverse direction and note the new reading at the same physical position. The difference is your backlash. On a 10:1 indicator, >0.0003 inches suggests excessive wear and may require disassembly or replacement. Some manufacturers offer anti-backlash models for critical applications.
Q: Are there any safety hazards when using dial indicators?
A: Yes. Over-tightening the mounting screw can strip the base or crack the dial face. Always use a torque wrench (typically 8–12 in-lbs for standard models). Additionally, flying debris from machining operations can damage the dial or spindle. In CNC environments, enclose the indicator with a clear shield or use a magnetic base to prevent accidental ejection during rapid movements.
Q: What’s the difference between a dial indicator and a bore gauge?
A: A bore gauge is a specialized dial indicator designed for internal diameter measurements, featuring a fixed base and an extendable stem. Unlike general-purpose indicators, bore gauges often include compensation for probe diameter and tapered contact points to ensure consistent readings in cylindrical bores. For example, a 2-inch bore gauge might have a 0.0001-inch least count but requires three-point contact to avoid conical errors.
