
The Complete Overview of Ultrasonic Cleaning with Mineral Spirits
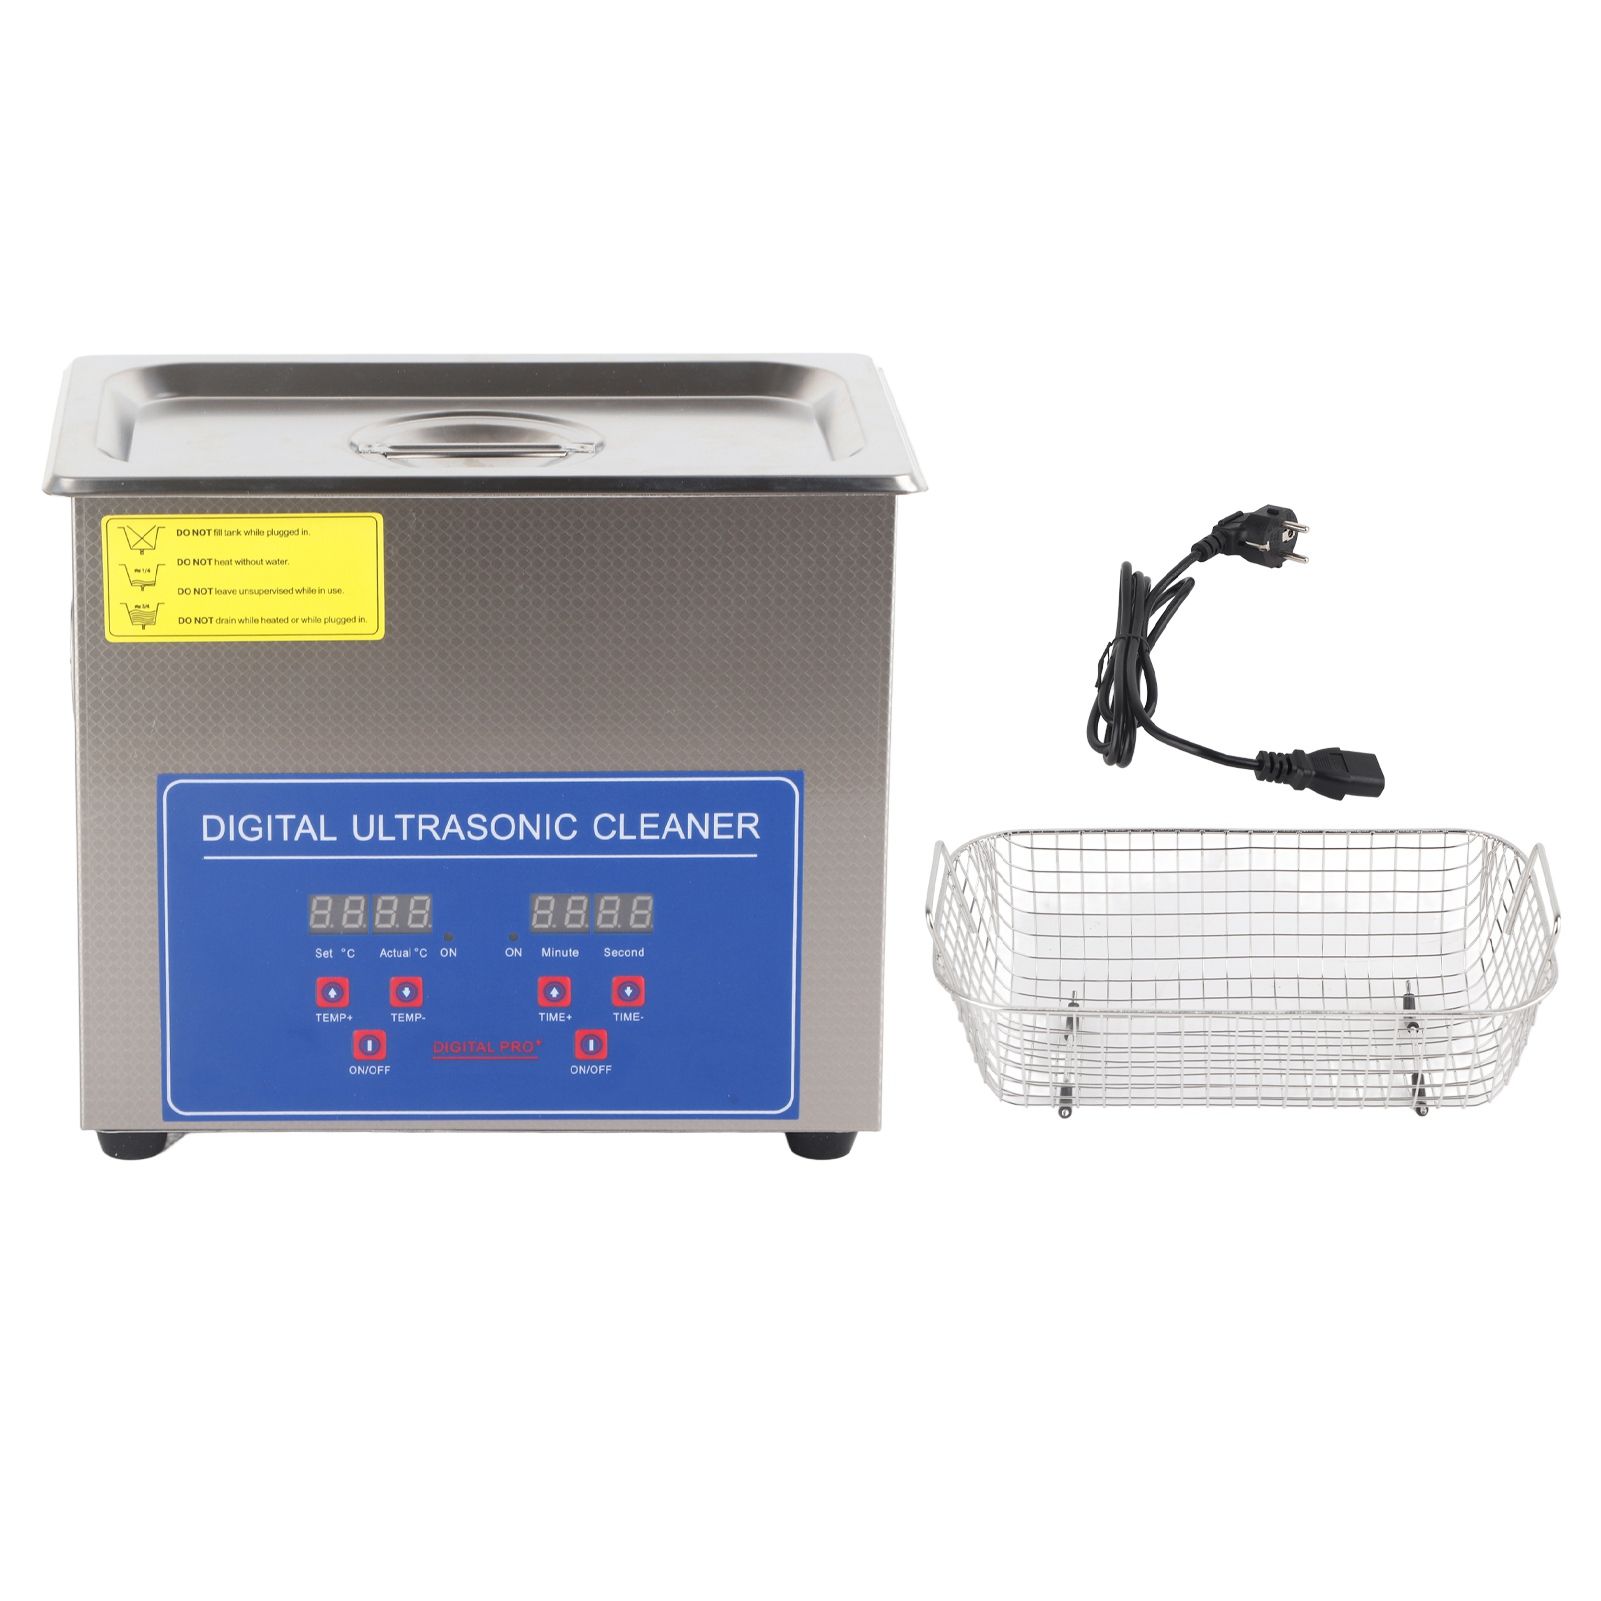
Ultrasonic cleaning with mineral spirits is a specialized process where high-frequency sound waves (typically 20–40 kHz) create microscopic cavitation bubbles in a solvent bath. These bubbles collapse violently, dislodging contaminants from metal, plastic, or delicate components—ideal for degreasing precision tools, firearms, or electronic contacts. But mineral spirits, with their lower boiling point (~150–200°C) and flammability, introduce critical variables. The temperature to run ultrasonic cleaner using mineral spirits must align with both the solvent’s chemical stability and the acoustic properties of the system. What distinguishes this method from water-based ultrasonics is the solvent’s role as both a medium and a reactant. Mineral spirits don’t just transmit sound—they dissolve oils and resins that water repels. However, their volatility means that exceeding recommended temperatures accelerates evaporation, increasing fire hazards and altering the cleaning chemistry. The interplay between heat, solvent properties, and ultrasonic energy creates a delicate equilibrium that demands precise control.Historical Background and Evolution
The marriage of ultrasonics and mineral spirits traces back to mid-20th-century industrial cleaning, when petroleum-based solvents became the gold standard for degreasing metal parts. Early ultrasonic cleaners, developed for military and aerospace applications, relied on mineral spirits for their ability to penetrate stubborn greases without leaving residues. By the 1970s, as environmental regulations tightened, alternatives like trichloroethylene emerged—but mineral spirits persisted in niche applications where solvent strength and low surface tension were non-negotiable. Today, the optimal temperature for ultrasonic cleaners using mineral spirits reflects decades of empirical refinement. Early systems often ran hotter (up to 60°C) to compensate for lower-frequency transducers, but modern 40 kHz+ units achieve superior cavitation at lower temperatures (30–45°C). The shift mirrors broader trends in precision cleaning: moving from brute-force heat to targeted energy efficiency. Yet despite advancements, the core principle remains unchanged—temperature dictates whether the solvent works with the ultrasonic waves or against them.Core Mechanisms: How It Works
Ultrasonic cleaning leverages acoustic cavitation, where rapid pressure changes create and collapse gas-filled bubbles. In mineral spirits, these bubbles form more efficiently than in water due to the solvent’s lower surface tension and higher vapor pressure. The temperature to run ultrasonic cleaner using mineral spirits directly influences bubble dynamics: colder baths (below 25°C) produce fewer, weaker bubbles, while excessive heat (above 50°C) can cause premature vaporization, reducing cavitation effectiveness. The solvent’s viscosity also plays a critical role. At lower temperatures, mineral spirits thicken, dampening ultrasonic energy transmission. Conversely, heating to 40–45°C lowers viscosity, improving wave propagation but risking solvent degradation if sustained. The sweet spot—where cavitation is maximized without compromising solvent integrity—typically falls between 35–40°C, though this varies by transducer type and part material.Key Benefits and Crucial Impact
Ultrasonic cleaning with mineral spirits isn’t just a technique—it’s a precision tool for industries where contaminants must vanish without trace. The method excels in removing embedded oils from firearms, restoring vintage watches, or cleaning semiconductor components where water would corrode or leave residues. Its efficiency lies in the synergy between ultrasonic energy and the solvent’s chemical properties, a combination that outperforms mechanical scrubbing or simple soaking. Yet the benefits come with caveats. Mineral spirits are classified as hazardous waste in many regions, and their flammability demands strict ventilation. The temperature to run ultrasonic cleaner using mineral spirits becomes a safety parameter as much as a performance one. Operators must balance cleaning efficacy with the risk of solvent vapor ignition, especially in enclosed systems. This duality—high performance with heightened risk—explains why the method remains niche despite its capabilities."You can’t optimize for speed alone when dealing with mineral spirits and ultrasonics. The temperature window is tight, and pushing it risks turning a $5,000 cleaner into a fire hazard—or worse, ruining parts you can’t replace." — Industrial Cleaning Specialist, Precision Maintenance Association
Major Advantages
- Superior degreasing: Mineral spirits dissolve oils and waxes that water repels, while ultrasonics dislodge particles at the microscopic level.
- Material compatibility: Safe for non-porous metals, plastics, and composites where water or alkaline solutions would degrade surfaces.
- Rapid cycle times: Effective cleaning often occurs in 5–15 minutes, compared to hours for manual methods.
- Residue-free results: Unlike aqueous solutions, mineral spirits leave no water spots or mineral deposits.
- Selective action: Can target specific contaminants without affecting underlying materials (e.g., cleaning gold-plated contacts without stripping the plating).
- Scalability: Systems range from bench-top units for jewelers to industrial tanks for aerospace components.
Comparative Analysis
| Parameter | Mineral Spirits + Ultrasonics | Water-Based Ultrasonics |
|---|---|---|
| Optimal Temperature Range | 35–45°C (varies by solvent blend) | 40–60°C (higher temps for alkaline additives) |
| Cleaning Efficiency for Oils/Grease | Excellent (solvent + cavitation synergy) | Moderate (requires detergents; may leave residues) |
| Safety Risks | Flammability, vapor hazards, disposal regulations | Corrosion potential, chemical handling (e.g., sodium hydroxide) |
Future Trends and Innovations
The future of ultrasonic cleaning with mineral spirits lies in two directions: sustainability and smart automation. As regulations tighten, alternatives like bio-based solvents or CO₂-based cleaners are encroaching on mineral spirits’ dominance. However, for applications where performance is non-negotiable—such as in semiconductor fabrication or vintage restoration—mineral spirits will persist, albeit with stricter temperature controls and closed-loop recovery systems. On the technical front, adaptive ultrasonic systems that adjust frequency and temperature in real-time could eliminate guesswork in determining what temperature to run ultrasonic cleaner using mineral spirits. Machine learning algorithms might analyze part material, contaminant type, and solvent batch to optimize cycles dynamically. Until then, operators will rely on a mix of manufacturer guidelines and in-house calibration—where experience often trumps data sheets.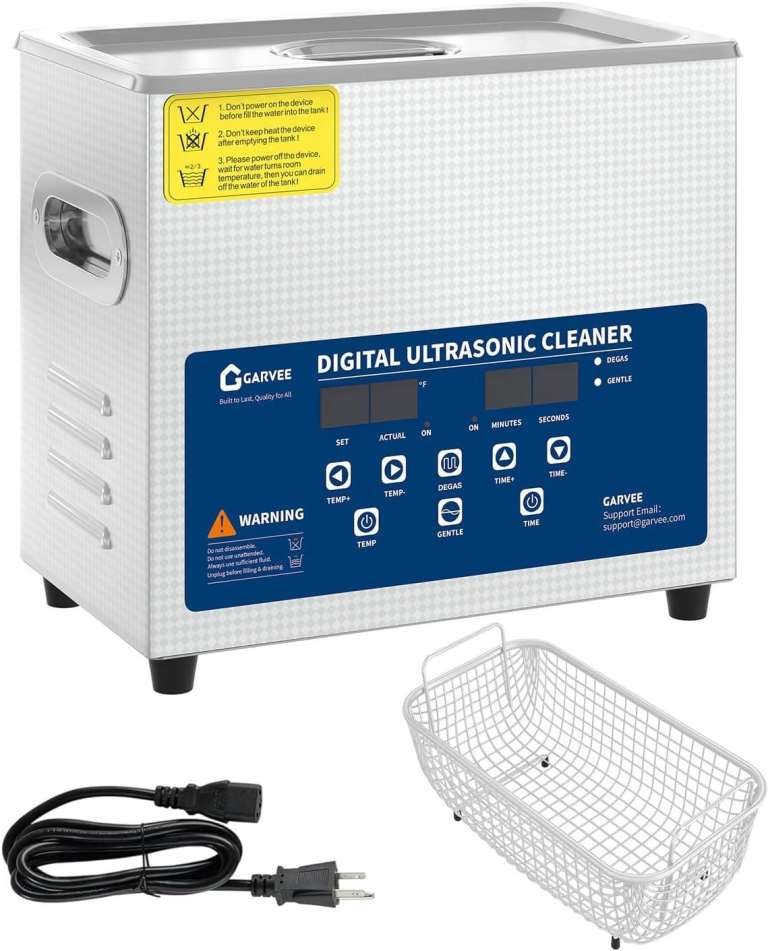
Conclusion
The temperature to run ultrasonic cleaner using mineral spirits is more than a setting—it’s the fulcrum between effective cleaning and operational failure. Ignore it, and you risk wasted solvent, damaged parts, or safety incidents. Master it, and you unlock a method capable of restoring precision instruments or preparing aerospace components with surgical precision. The challenge lies in treating temperature as a variable, not a constant: adjusting for ambient conditions, solvent batch variability, and the specific demands of the part being cleaned. For practitioners, the key takeaway is this: mineral spirits and ultrasonics demand respect for their chemistry. The optimal temperature isn’t a fixed number but a range informed by real-time monitoring and iterative testing. As the industry evolves, those who treat this balance as an art—not just a science—will continue to outperform competitors relying on outdated assumptions.Comprehensive FAQs
Q: What’s the safest temperature range for ultrasonic cleaning with mineral spirits?
Most industry sources recommend 35–40°C as the safest operational range. Below 30°C, cavitation weakens; above 45°C, vapor pressure increases fire risks and accelerates solvent degradation. Always consult your solvent’s MSDS for precise flashpoint data.
Q: Can I use a higher temperature to speed up cleaning?
Not safely. While higher temperatures (e.g., 50°C+) may seem to improve cleaning speed, they increase solvent evaporation, reduce cavitation efficiency, and elevate fire hazards. Mineral spirits’ flashpoint (~38°C closed cup) means even slight overheating can create explosive vapor-air mixtures.
Q: Does the transducer type affect the optimal temperature?
Yes. Lower-frequency transducers (20–25 kHz) often require slightly higher temperatures (up to 45°C) to maintain cavitation, while higher-frequency units (40 kHz+) can operate effectively at 30–35°C. Always check the manufacturer’s specifications for your specific ultrasonic cleaner model.
Q: What happens if I run the cleaner too cold?
At temperatures below 25°C, mineral spirits become too viscous, dampening ultrasonic waves and reducing cavitation. Cleaning effectiveness drops significantly, and longer cycles may not fully remove contaminants—potentially leaving residues that could interfere with subsequent processes.
Q: Are there additives that can adjust the optimal temperature range?
Some specialized mineral spirit blends include cavitation enhancers or stabilizers that allow slightly lower operating temperatures (e.g., 30–35°C). However, these additives must be compatible with your ultrasonic system and the parts being cleaned—always verify with the supplier.
Q: How does humidity affect the temperature settings?
High humidity can lower the effective flashpoint of mineral spirits, increasing fire risks even at standard operating temperatures. In humid environments, it’s critical to monitor solvent levels and adjust temperature settings conservatively (staying below 40°C) to prevent vapor buildup.
Q: What’s the best way to monitor temperature during a cycle?
Use a digital thermometer with an immersion probe placed in the solvent bath, away from the transducer. Avoid relying on the cleaner’s display if it hasn’t been recently calibrated. For critical applications, consider a dedicated temperature controller with alarms for deviations.
Q: Can I reuse mineral spirits after ultrasonic cleaning?
Reuse is possible but requires careful monitoring. Evaporation and contamination (e.g., dissolved oils) alter the solvent’s properties over time. If the temperature was consistently above 40°C, the solvent may degrade faster. Test a small batch first—if cleaning efficacy drops or the solvent smells acrid, replace it.
Q: What’s the most common mistake with temperature settings?
Assuming a one-size-fits-all approach. Many operators default to the highest recommended temperature to "ensure" cleaning, unaware that this accelerates solvent breakdown. The temperature to run ultrasonic cleaner using mineral spirits should be tailored to the specific solvent blend, part material, and contaminant type—not treated as a static value.
